The demethanizer separates methane from the C₂ and heavier hydrocarbons, recovering ethane in gas processing and ethylene in an olefins plant. In an ethylene plant it sits where the plant's most energy-intensive operation meets its most composition-sensitive separation. The IEA identifies the chemical sector as the largest industrial energy consumer, which makes the demethanizer one of the highest-impact columns for operational improvement.
It is also hard to optimize because its best operating point keeps moving. Feed conditions change with feedstock variability, ambient temperature and upstream upsets. The best pressure, reflux and heat integration settings at 6 a.m. may not be the best settings by noon.
How the demethanizer shapes downstream recovery
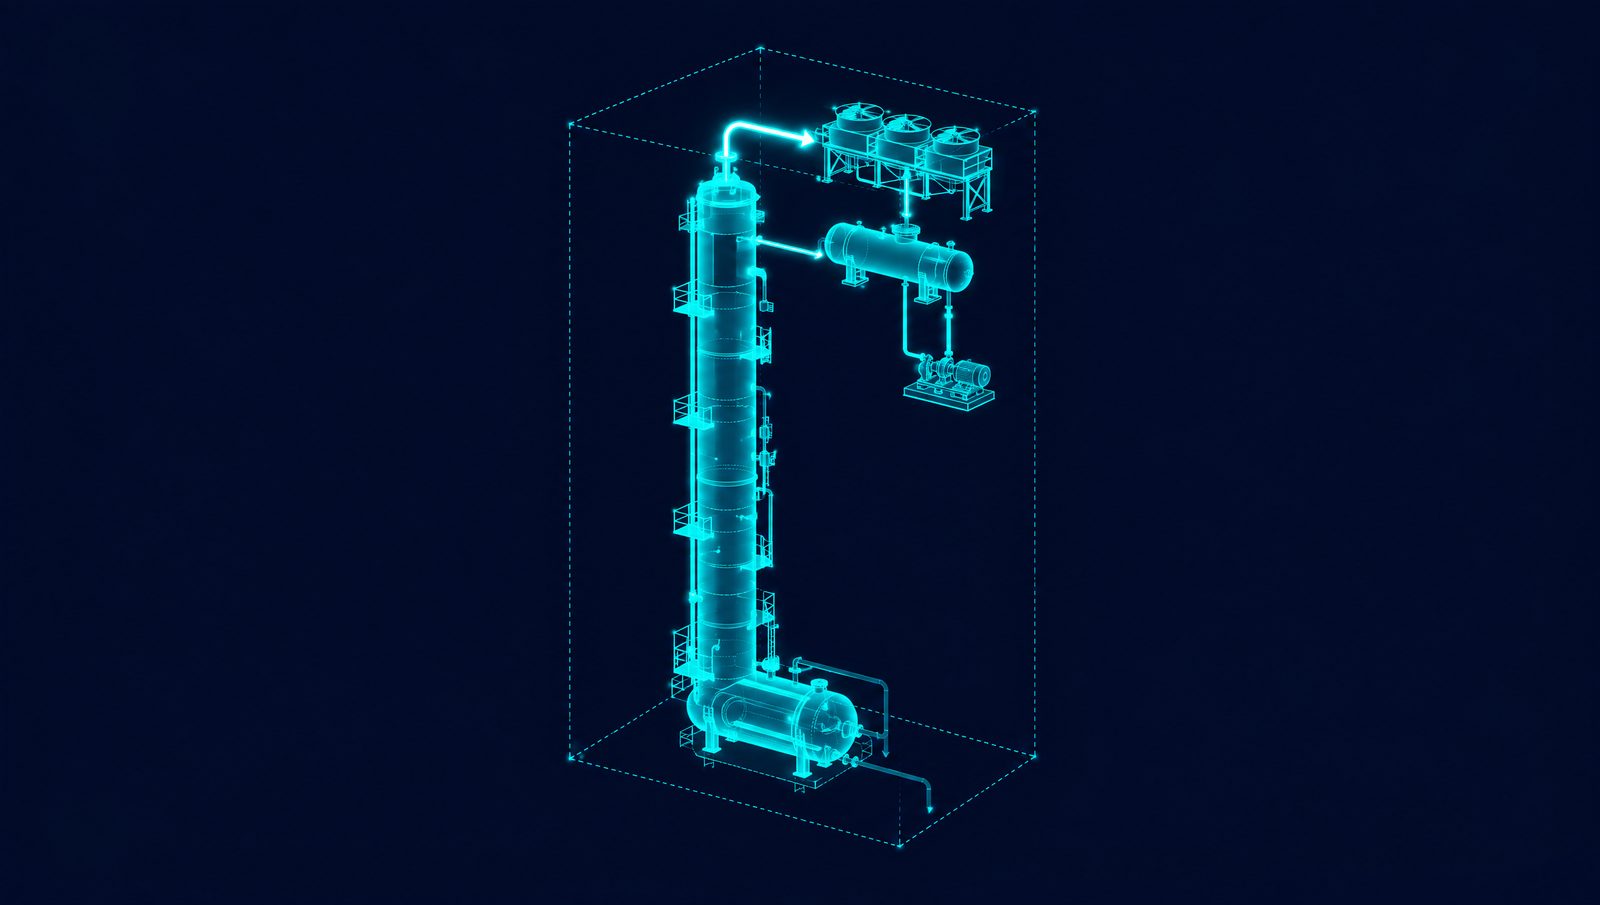
The demethanizer uses the volatility difference between methane and the C₂ components at cryogenic temperatures to drive the separation. That difference narrows as column pressure rises, and the column is tightly coupled to the refrigeration system, so it is more sensitive to shifts in operating conditions than most others in the plant.
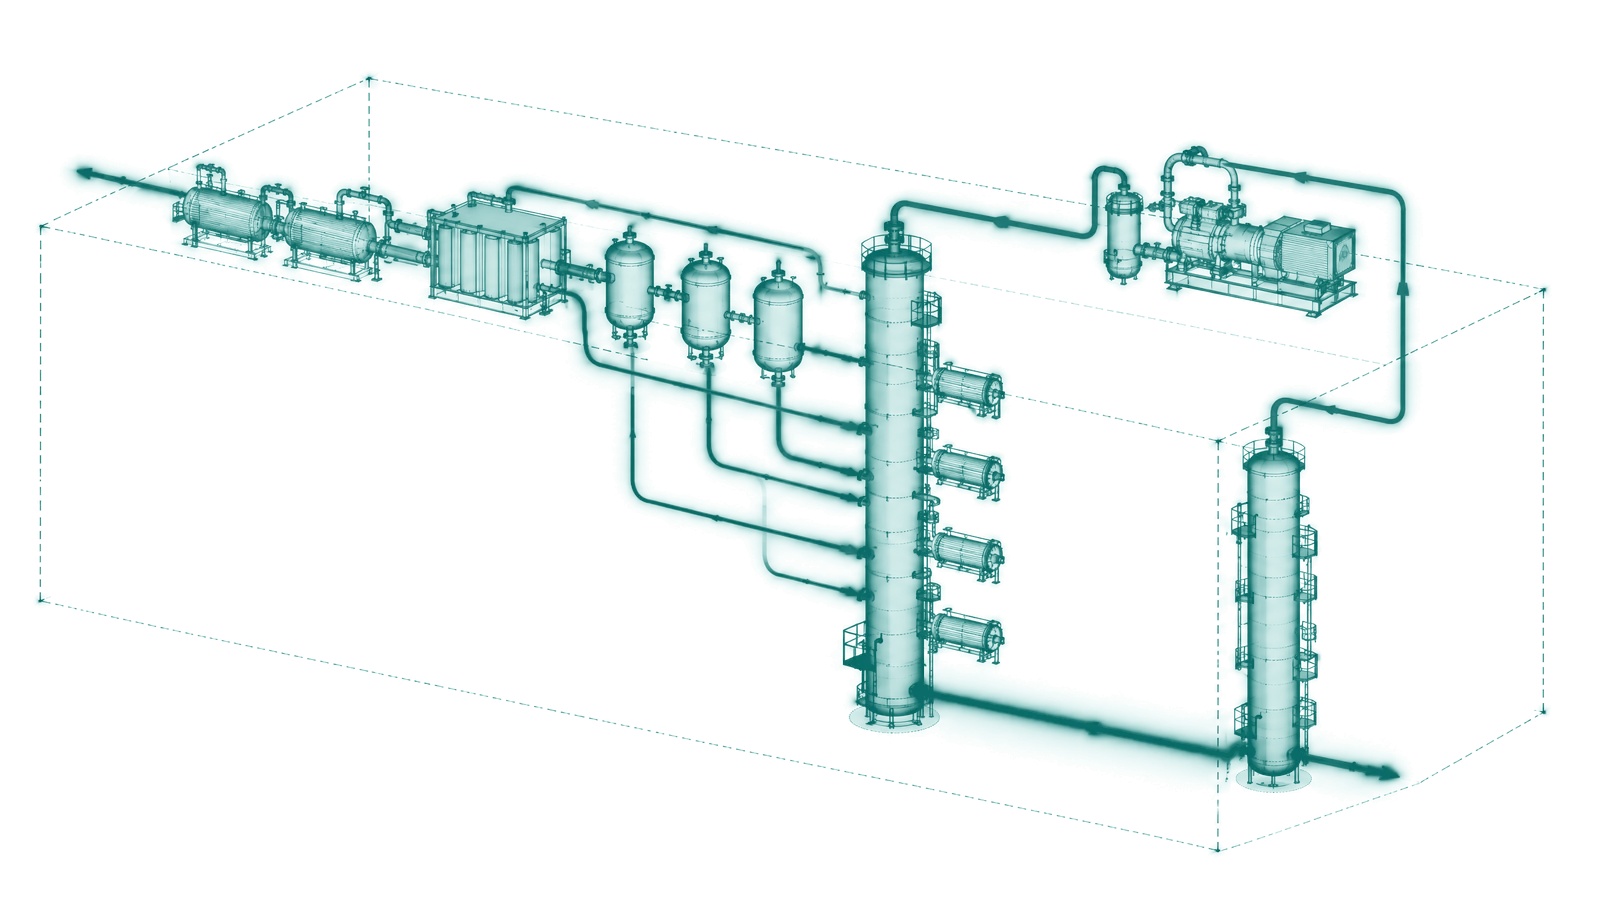
In an ethylene plant, the column follows multistage cracked gas compression, caustic washing and molecular sieve drying. The cold box serves as its condenser and integrates heat recovery across the chilling train. That tight integration means the column's operating conditions directly affect refrigeration system performance and compressor loading across the cold side of the plant.
Its position in the olefins separation train means separation quality here matters well beyond one column. Downstream columns, including the depropanizer, depend on the quality of the demethanizer bottoms. Poor methane-ethane separation carries through to recovery across the fractionation sequence, to column loading and to plant economics.
How pressure, reflux and heat integration trade energy against recovery
Column pressure
Column pressure is the primary design variable. It sets relative volatility, vapor loading limits, the temperature profile and even material specifications. Feed composition changes can shift the pressure that best balances recovery and energy use, so a fixed pressure is often suboptimal across the range of feeds a plant actually runs.
The trade-off is direct:
- Higher pressure reduces refrigeration duty but compresses the methane-ethane relative volatility, which makes the separation harder.
- Lower pressure makes the separation easier but demands colder overhead temperatures, more refrigeration capacity and potentially low-temperature alloy steel.
Reflux ratio
Reflux interacts with both sides of that trade-off. Higher reflux improves recovery but raises condenser duty and refrigeration load. Pressure optimization can improve recovery while reducing energy consumption, which reflux alone cannot do. That changes which lever operators should reach for first when feed conditions shift.
Heat integration
Heat integration is where the largest energy savings sit. Side reboilers let the demethanizer provide refrigeration to its own feed system, which eliminates or minimizes external propane refrigeration. Multiple feed entry points, split through flash separators at different pressures, let engineers match each entry to the column's internal composition profile and reduce condenser duty.
Combined levers
Pressure, reflux, feed handling and heat integration settings together can materially reduce compressor shaft power with no capital expenditure. The benefit depends on the unit's current constraints and feed. Whether a cracker runs an ethane-heavy or a naphtha-heavy feed slate changes the column's composition profile and moves the pressure at which recovery and energy balance.
On a unit that already dominates the plant's refrigeration load, even small pressure adjustments can change energy consumption by several percent. Many facilities revisit these settings only at turnarounds or major feed slate changes. Treating them as fixed design parameters instead of adjustable operating levers leaves recoverable margin between those events.
Why operating constraints make static setpoints unreliable
CO₂ freeze-out, flooding, heat exchanger fouling and ambient temperature all shift the optimal operating point, often several times a day, and they interact.
CO₂ freeze-out
CO₂ can form dry ice in the column's coldest sections. When feed CO₂ content changes, a plant may have to cut recovery repeatedly to stay clear of freeze-out. Holding recovery safely requires adjusting pressure, vapor-liquid splits and reboiler duty together.
Heat exchanger fouling
Fouling reduces exchanger UA continuously and nonlinearly, so feed arrives progressively warmer than design. The temperature profile shifts, which forces either more refrigeration load or lower recovery. C₂+ recovery can degrade even when every other variable looks normal.
Fouling also misleads diagnosis. In severe cases, thermosiphon reboiler problems produce symptoms that resemble hydraulic flooding. Because fouling develops gradually, the loss can go unrecognized until the cumulative cost is significant. Advanced process control (APC) models calibrated at commissioning become less accurate as these conditions drift.
Ambient temperature and compression
At some facilities, the available compression horsepower changes with cooling water performance. On hot afternoons, reduced horsepower forces operators to raise demethanizer pressure or cut throughput. The temperature effect on compression capacity builds over hours, so operators may not see that the constraint has shifted until the end-of-shift recovery numbers show it.
Migrating bottlenecks
The throughput bottleneck itself moves. It may sit at the demethanizer, the refrigeration system or the compressor, and it shifts with feed changes, the number of furnaces online and the weather. APC configured for one bottleneck location can become counterproductive when the bottleneck moves.
Experienced board operators develop a sense for which constraint is active, but that judgment depends on recognizing patterns across dozens of variables at once. These interacting constraints make the demethanizer one of the hardest columns to optimize with conventional process control.
What continuous optimization looks like in operation
A model learned from the plant's own data does not rest on a fixed process model from commissioning. When it finds that the current feed composition favors lower column pressure with adjusted reflux splits, that finding reaches board operators, planners and engineers at the same time. Planners can update recovery assumptions, and engineers can quantify the energy penalty of current fouling levels.
That shared view matters because these groups often work apart. Operations responds to current constraints, planning works from recovery assumptions, and engineering evaluates longer-term changes. Changing a recovery target moves column hydraulics, temperature profiles and product specifications at once, so pressure, reflux and feed split changes have to be considered together. When all three groups see the same process behavior, they respond to the same constraint instead of making separate decisions from different models.
How trust builds toward closed loop
Plants usually start in advisory mode: the model recommends setpoint changes and operators decide whether to act. Advisory mode also gives every shift the same reference and helps planning evaluate changing constraints.
On a demethanizer, trust depends on diagnosis. CO₂ freeze-out, flooding and fouling can produce similar symptoms, so operators need to see the model identify the active constraint correctly before they give it more authority. Newer operators learn from the same diagnostic reasoning, which builds their pattern recognition faster and makes knowledge transfer more practical as experienced staff retire from cryogenic operations.
As trust builds, plants move from advisory recommendations to operator-approved execution and then to closed-loop control, with the model writing setpoints to the distributed control system (DCS) inside limits the operators set. Authority does not have to move all at once. A plant can keep CO₂-sensitive operation in advisory mode while closed-loop control handles reflux optimization during stable periods. Throughout, operators and the model work together, with operators able to take over from the board.
How the Imubit Platform applies
Imubit applies Map, Model and Control to the demethanizer and the wider olefins fractionation train as part of its work in chemicals and polymers. Map traces lost ethylene recovery and excess refrigeration energy to the recurring decisions behind them, such as column pressure, reflux and feed split targets. Model uses Deep Learning Process Control® (DLPC®) to learn the column's nonlinear behavior, and its coupling to refrigeration and compression, from its own history, guided by first principles. Control takes those decisions to closed loop, writing setpoints to the existing APC and DCS, inside limits set by plant engineers.