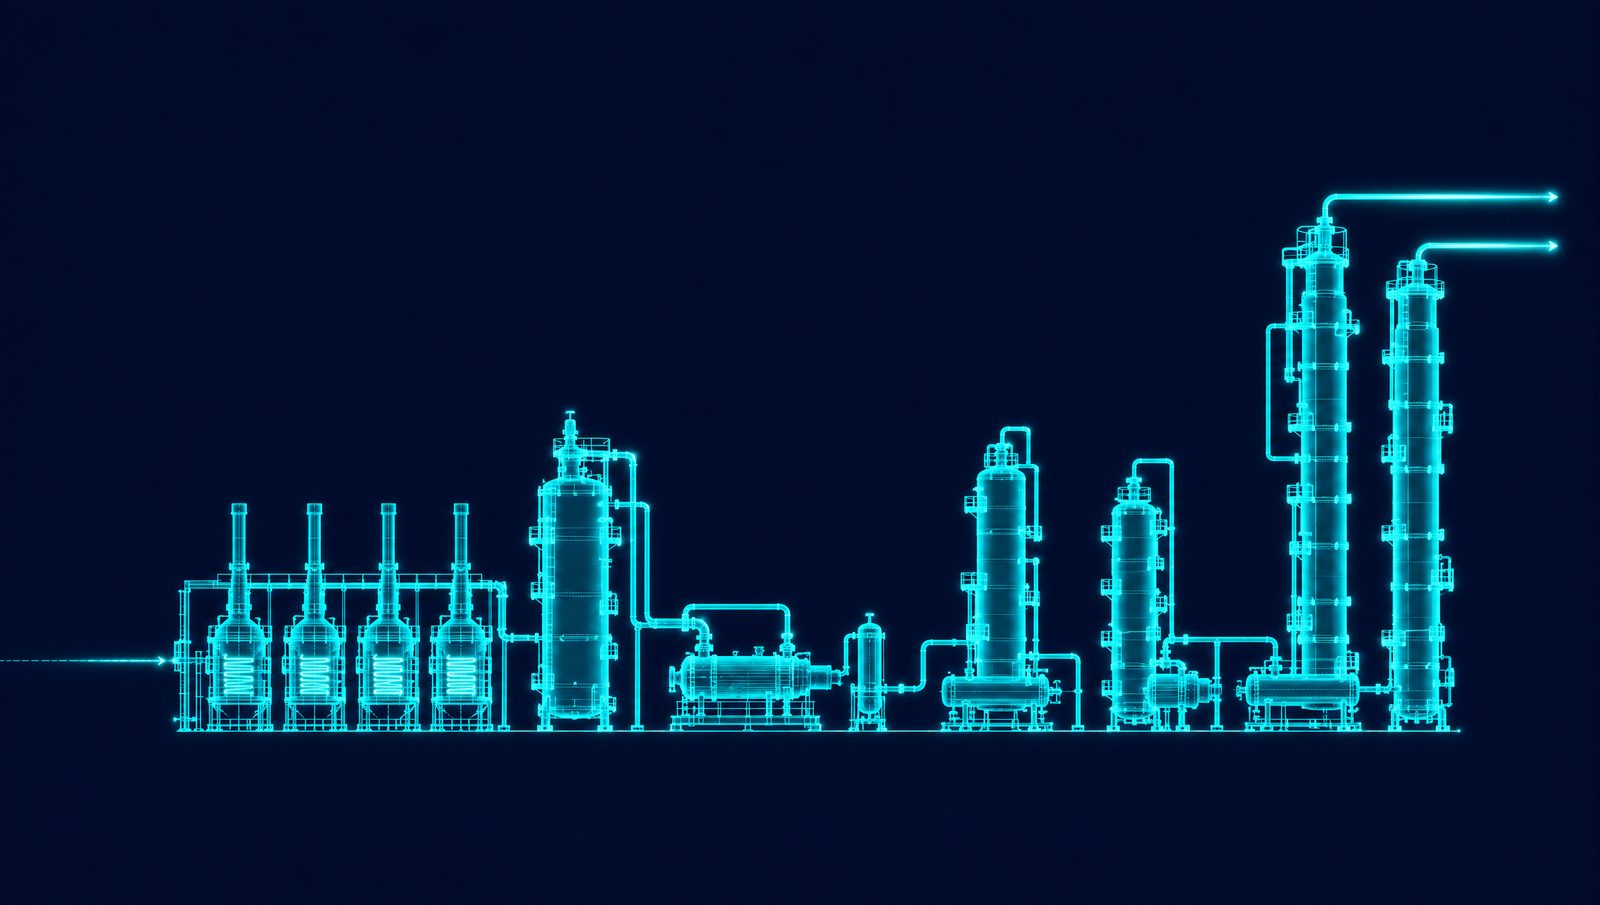
Every olefins plant runs the same basic chemistry. Feed enters the furnace, cracks into lighter hydrocarbons, and moves through quench, compression and fractionation until polymer-grade ethylene and propylene come out the other end. Profitability depends on how well each stage connects to the next.
Feedstock is a large share of operating cost, so every point of yield, every hour of unplanned downtime and every degree of temperature variability carries financial weight. Margin recovery starts with knowing where the losses sit.
How feedstock choice sets the product slate
The product slate an olefins plant can offer starts with what goes into the furnace. Ethane-rich feeds favor ethylene but produce little propylene, C4 olefins or aromatics. Naphtha feeds give a lower ethylene yield and more co-products, which can partly offset their higher cost.
That co-product balance shapes economics as much as chemistry does. When ethylene margins compress but propylene or butadiene markets strengthen, a naphtha cracker can shift severity toward a more valuable product mix. An ethane cracker has much less room to do that.
A plant built around C3 and C4 by-products cannot switch to a lighter feed and expect the same economics. Feed flexibility is becoming a design goal for new plants, but for most existing crackers the feed envelope is already set. Within it, operations controls margin through yield, throughput and reliability, and managing feedstock variability becomes an operating discipline as much as a planning exercise.
Feed choice affects the plant long after the furnace inlet. Separation loads, compressor behavior, hydrogenation selectivity and co-product recovery all move with the feed. A feed that looks attractive on headline ethylene yield can still tighten operating windows downstream. In many plants, margin recovery comes less from changing the feed slate than from running the current one with less variability.
How furnace conditions shape everything downstream
The cracking furnace sets olefins plant economics. Feed enters the convection section, mixes with dilution steam and preheats before it reaches the radiant section. There the temperature rises sharply, and residence time is kept deliberately short to limit the secondary reactions that degrade yield.
Coil outlet temperature (COT) is the main severity lever. Raising COT can improve ethylene yield, and higher severity pays when the added olefins are worth more than the shorter run length and extra decoking it brings. The cost is that coking accelerates as severity rises.
COT variability matters as much as the setpoint. Coke formation generally increases with temperature, so pass balancing is critical to holding target run length.
Coke progression and decoking timing
When individual passes run at different severities, the hottest pass sets the decoking schedule for the whole furnace, even if the other coils still have useful life. As coke builds on the tube walls, it insulates the process from the firebox. Tube metal temperature rises, firing gets harder and deposition can accelerate. Eventually the furnace comes offline for decoking, and that outage cuts directly into production.
Run length varies between decoking cycles for the same reasons. Tube metal temperature progression, dilution steam ratio, feed composition and firing rate all affect when a furnace must come offline. When those variables are managed independently, some passes reach their limit early and force decoking of the whole furnace while the rest of the coil set is still manageable.
The dilution steam ratio adds another trade-off for cracking furnace efficiency. More steam can suppress coking, but it raises furnace energy use. Finding the right balance for each furnace, each feed and each margin environment is a daily operating problem that static setpoints rarely handle well.
The hard part is holding the target as feed quality shifts, ambient conditions move and individual passes drift apart over the run. Operators see the interaction directly, because small severity changes at the furnace often reappear later as instability in compression and fractionation.
How compression and fractionation become margin leaks
Once cracked gas leaves the furnace and quench system, it enters a compression and separation chain where small inefficiencies compound into larger losses.
Cracked gas compression
The cracked gas compressor is often the most critical rotating asset in the plant. It typically has no spare, and a trip can force a broad production interruption. Fouling matters because it reduces compressor efficiency, and because it can contaminate downstream equipment and disturb the rest of the separation train. Monitoring surge margin gives operations early warning before a constraint forces corrective action.
Separation train losses
In the separation section, the demethanizer, deethanizer and C2 splitter must hold tight product specifications while keeping energy use in check. Lower demethanizer pressure improves ethylene recovery but can raise total energy demand, and operational or thermodynamic constraints often limit how low that pressure can go. Acetylene hydrogenation is another recurring yield leak, because over-hydrogenation converts valuable ethylene to ethane.
For naphtha crackers, the C3 splitter is especially energy-intensive because propylene and propane boil so close together. Vapor recompression can reduce energy demand, but the column still has to stay inside a narrow hydraulic envelope bounded by flooding on one side and weeping on the other.
These losses rarely show up as a single dramatic event. More often they appear as small specification cushions, conservative pressure targets, extra reflux or operating choices made to avoid instability after the last upset. Each choice is understandable on its own. Across the full train, together they can leave a meaningful amount of yield and energy performance unrealized.
Where conventional optimization reaches its limit
Advanced process control (APC) has delivered real value in olefins operations. Plants have reduced furnace hot spots and pushed closer to constraints with better control discipline. The limit is that APC typically works from linear models, while olefins plants behave in strongly nonlinear ways.
The relationship between COT, dilution steam ratio and ethylene selectivity shows the problem. Those variables interact with each other, and a linear model approximates that interaction at best. When planning uses linear programming and operations relies on linear APC models, each group works from a different version of plant behavior.
The gap between planning and the board
That gap shows up across teams every day. Planning sets targets from steady-state assumptions. Operations adjusts for the constraints visible in the moment. Maintenance often schedules decoking from historical intervals instead of current tube condition. A shared model of how the plant behaves gives those functions a common basis for discussing throughput, run length and yield trade-offs, which is the core of chemical manufacturing optimization.
Without constraint automation, operators usually hold the process farther from hard limits to preserve operating margin. That caution is rational at the board, but across shifts, furnaces and changing feed it leaves capacity and yield unrealized. No optimization technology substitutes for the pattern recognition that comes from decades at the board. Holding the process near constraint boundaries around the clock is still hard for any team, especially as experienced operators retire and newer staff take on more responsibility.
Measuring where variability costs margin
The most useful measures show how far day-to-day operation sits from the economic limit:
- shift-to-shift variability in COT and severity targets
- average distance from equipment limits such as tube metal temperature and column flooding
- the gap between planned and actual yield
Tracked across furnaces, compression and fractionation, they show whether losses come from conservative operation, inconsistent execution or true equipment effectiveness constraints.
How learned models build trust in daily operation
A model learned from operating history works differently from a linear controller. It captures how the furnaces and columns respond across feedstock regimes, and it connects process setpoints to economic targets as well as to fixed process limits.
Starting in advisory mode
Trust usually starts in advisory mode. The model recommends setpoint changes, and operators decide whether those changes fit what they see in the unit. Experienced operators can test recommendations against their own judgment, field observations and known equipment constraints, and newer operators get a clearer view of how constraints move together.
Advisory mode also improves consistency across shifts. Instead of each crew interpreting the same trade-off differently, the plant gets a common reference for what current conditions imply. That supports operator training by making the relationships between furnace, compression and fractionation variables visible in a way that manual board operation rarely does.
Moving to closed loop
When the model repeatedly reflects relationships the team recognizes and surfaces useful moves, it becomes part of daily decision-making instead of an outside system operators are asked to accept on faith. The plant then moves to closed loop, with the controller writing setpoints to the APC or DCS inside limits the operators set. That is the path toward a self-optimizing petrochemical plant.
How the Imubit Platform applies
In chemicals and polymers, the Imubit Platform applies Map, Model and Control to the furnace, compression and fractionation decisions that set olefins margin. Map traces the gap between the plan and the plant to the recurring decisions behind it, such as COT targets, dilution steam ratio, decoking timing and separation pressures. Model uses Deep Learning Process Control® (DLPC®) to learn a nonlinear dynamic model of each section from the plant's own history, guided by first principles. Control takes the critical decisions to closed loop, writing setpoints to the existing APC and DCS minute by minute, inside limits set by plant engineers.