Nearly every barrel of crude a refinery processes passes through at least one fired heater before it reaches a distillation column, a hydrocracker or a reformer. According to the U.S. Department of Energy's petroleum refining bandwidth study, process heating accounts for roughly two-thirds of fuel use in petroleum refining, which makes fired heaters the largest fuel consumers on most sites.
When a furnace underperforms, the effects travel across the plant. Fuel use climbs, throughput drops, tube-metal temperatures rise toward creep limits, and an unplanned shutdown takes margin from every unit the heater feeds. Yet many refineries still run furnaces reactively, addressing fouling, flow imbalance and lost efficiency only after performance has visibly declined. A better path combines disciplined operating practices with learned models that detect problems early and adjust firing continuously.
How a refinery furnace works
A refinery furnace, also called a fired heater or process heater, raises hydrocarbon streams to the temperatures needed for downstream separation or reaction. Crude distillation, vacuum distillation, hydrocracking, catalytic reforming and coking all depend on fired heaters to deliver precise outlet temperatures.
Radiant and convection sections
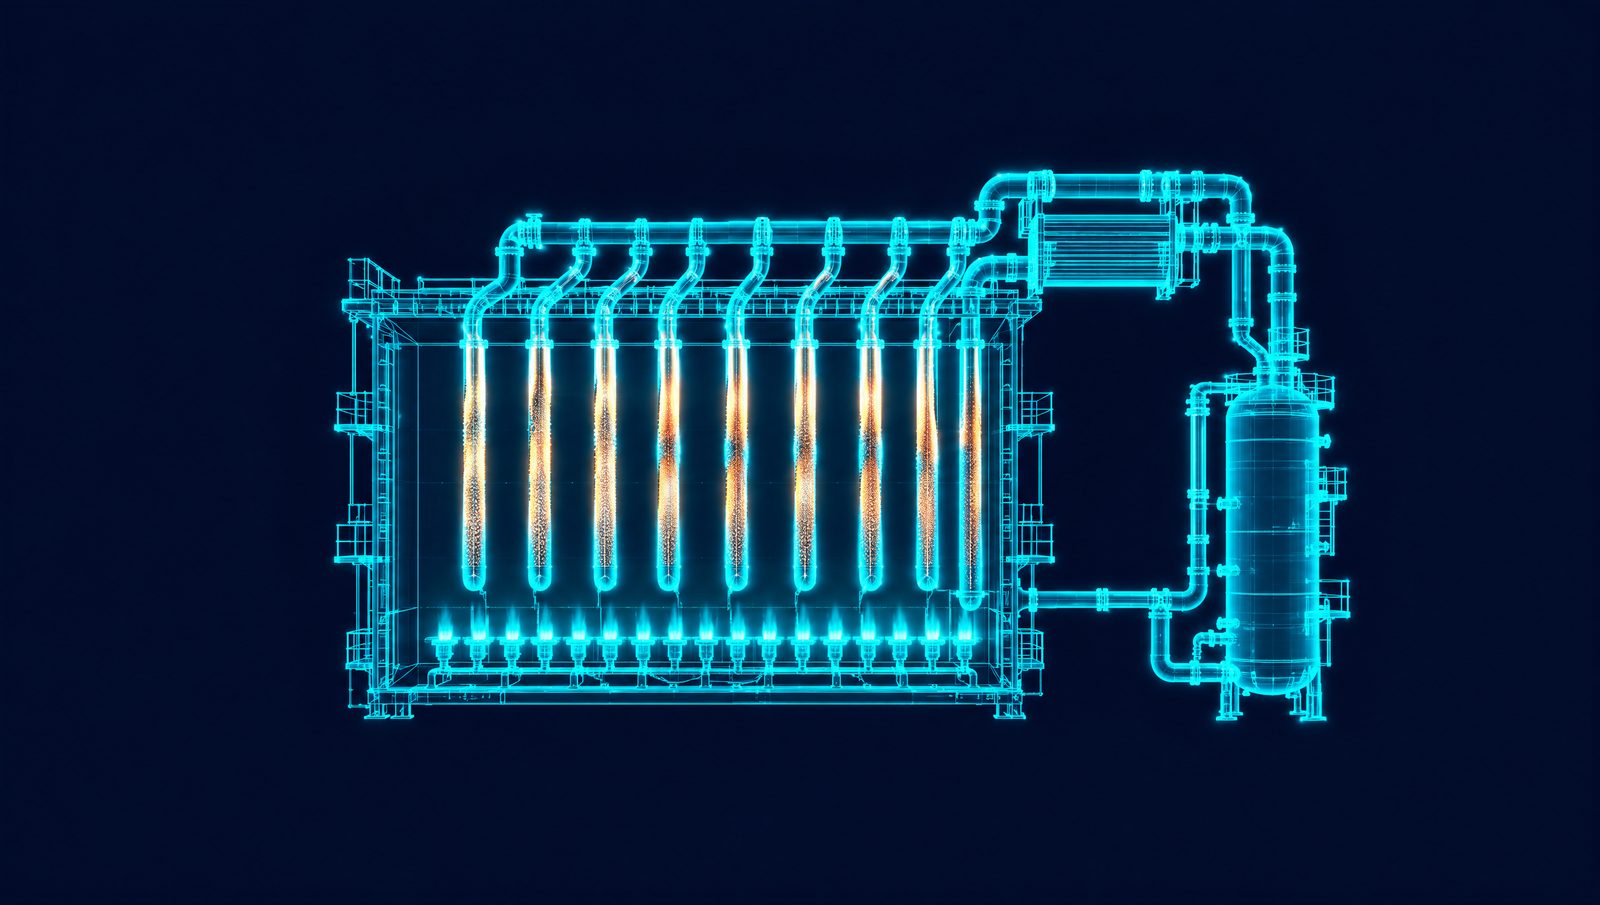
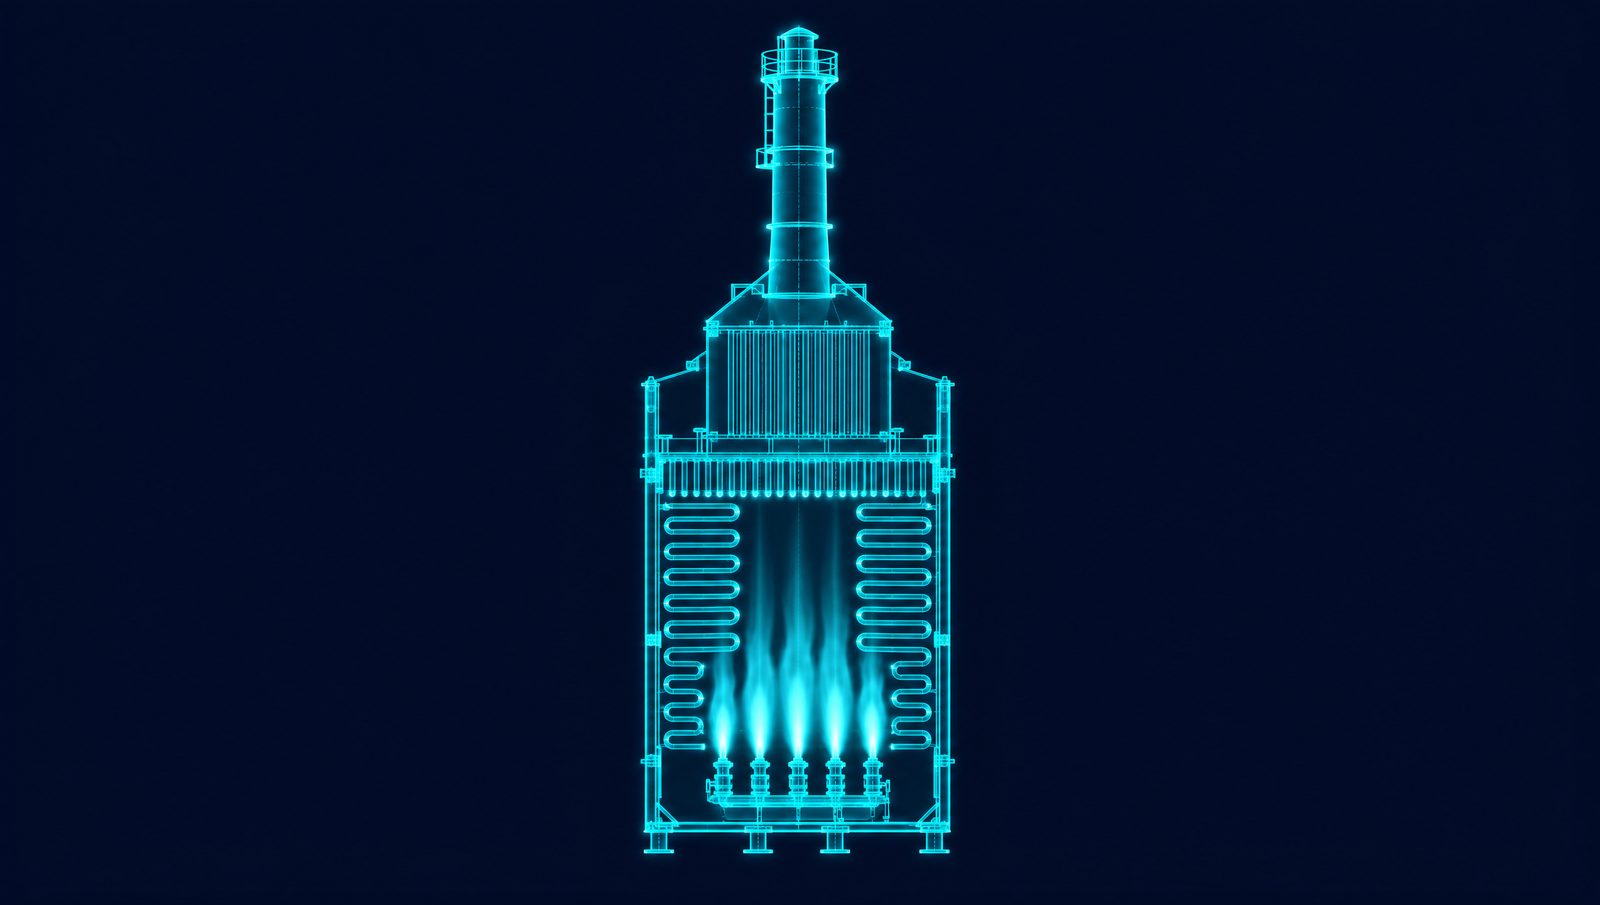
The furnace has two main heat transfer zones. In the radiant section, burners combust fuel gas or refinery gas, and the flames transfer energy mainly by radiation to the process tubes lining the firebox walls. Tube-metal temperatures here are the highest anywhere in the heater, which makes this section the most vulnerable to overheating and coke accumulation.
Above it sits the convection section, where hot flue gas gives up residual heat to additional tube banks before leaving through the stack. Finned tubes in this zone recover energy that would otherwise be lost. Between the two zones, bare shield tubes protect the convection bank from direct flame radiation. In well-maintained units, overall thermal efficiency typically reaches 85 to 92%.
Draft control, excess air management and burner tuning all influence how efficiently fuel becomes useful process heat. Small deviations, such as air infiltration or uneven burner flames, can cost several percentage points of efficiency and add to fuel use over the length of a run.
What degrades a refinery furnace
Furnace degradation rarely comes from one dramatic event. It accumulates through daily operating habits that erode heat transfer, raise tube-metal temperatures and shorten the interval between turnarounds. A few patterns account for most premature failures.
Pushing through fouling instead of addressing it
When outlet temperature drifts or dampers creep open, the instinct is to fire harder to hold throughput. That puts more heat into tubes that are already compromised. Coke growth inside the coils and ash deposits on the fireside accelerate in response.
Fouling deposits act as insulation between the flame and the process fluid. Even a thin layer can degrade heat transfer enough to push tube-metal temperatures toward the alloy's creep limit. The furnace burns more fuel to reach the same outlet temperature, stack temperature rises, and coke forms faster. Plants that trend skin thermocouple data and schedule cleaning on fouling indicators rather than calendar intervals tend to break this cycle before it shortens a run.
Allowing uneven pass flows
Multi-pass furnaces depend on balanced flow to keep heat transfer uniform. When one pass becomes restricted, through worn orifice plates, fouling or misalignment after maintenance, the remaining passes absorb a disproportionate share of the heat. Tube-metal temperatures spike locally, and coking accelerates in the restricted pass.
These imbalances often hide behind a steady combined outlet temperature, so they stay invisible without per-pass monitoring. Recalibrating flow instruments at turnaround and alarming on pass-to-pass deviations outside normal bands are reliable ways to catch them early.
Missing early warning signals
A slight increase in pressure drop, a one-degree drift in outlet temperature or a slow rise in stack temperature often appears days or weeks before severe fouling develops. A furnace involves hundreds of interacting variables, and the fouling signature develops in the correlations between feed composition, draft, excess air and downstream conditions.
Trend charts of individual readings cannot pick out these multivariable patterns from normal operating noise. By the time a hot spot shows on a thermal scan, tube damage is already under way. Rate-of-change alarms can surface drift in single parameters, but the cross-variable patterns behind degradation exceed what manual monitoring can sustain.
Running the furnace in isolation from the rest of the plant
A crude or vacuum heater's stability depends on steady feed properties, balanced downstream draws and consistent combustion. When a distillation column cuts rates suddenly or a downstream unit goes off specification, the heater absorbs fast swings in flow and firing demand. Those abrupt transitions drive tube-metal temperatures above safe limits and encourage coking. The root cause is often organizational: each operator optimizes their own unit without visibility into constraints elsewhere in the refinery.
Why conventional furnace control falls short
Consistency across shifts compounds the detection problem. Each crew reads furnace data differently, setpoints drift between handovers, and institutional knowledge erodes as experienced staff retire. Documented procedures help, but no team can hold that level of attention on dozens of variables per heater across every shift.
Conventional advanced process control (APC) closes part of the gap by adjusting setpoints within predefined models. Those models rest on linear assumptions that hold well in steady operation and weaken as fouling progresses and conditions drift from design. A model tuned for a clean heater early in a run may underperform months later, once coke deposits have changed the heat transfer characteristics. Retuning mid-run is rarely practical, so operators often override the controller and return to manual adjustment. The nonlinear, time-varying dynamics of furnace degradation call for a different modeling approach.
How learned models extend furnace run length
A model trained on the heater's own operating history can capture those nonlinear relationships. It learns how combinations of feed rate, firing intensity, pass flow distribution and ambient conditions affect tube-metal temperature and fouling progression in that particular unit, and how fouling will shift the best setpoints over the following weeks.
The model works on top of the existing APC and control system. Existing control loops continue to handle low-level regulation, while the model adjusts the higher-level targets as conditions evolve.
Building trust with recommendations
Many plants begin with recommendations. The model presents setpoints with their expected effect, so plant operators can see why a firing adjustment makes sense before accepting it. At this stage it already gives crews fouling trajectory forecasts to inform cleaning schedules, what-if analysis for different crude slates, and a consistent reference that watches every variable on every shift.
Shared visibility across teams
When teams work from one model of the furnace's behavior, coordination across functions improves. Planning can evaluate how different crude slates affect fouling rates. Operations can see how downstream rate changes will carry into heater duty. Maintenance can time cleaning on predicted degradation rather than a fixed schedule. Shared visibility reduces the finger-pointing that tends to follow furnace-related shutdowns and speeds decisions when conditions change.
From recommendations to closed loop
Operators bring judgment from years of reading a furnace that no model reproduces. The model handles what is hard for any crew: tracking hundreds of variables at once, picking faint signs of an emerging imbalance out of normal noise, and holding the same standard on every shift. As trust builds, the model moves to closed loop and writes setpoints to the distributed control system (DCS) within limits the operations team sets, with operators able to take over at any time. The aim is lower fuel intensity and longer tube campaigns, sustained over the whole run.
How Imubit applies this
In refining, Map traces fuel and run length lost at the heater to the recurring decisions behind them, such as firing harder through fouling or crude slates chosen without their effect on fouling. Model learns the heater's nonlinear behavior from its own history with Deep Learning Process Control® (DLPC®). Control takes those decisions to closed loop on top of the existing APC and DCS, inside limits set by plant engineers. On one refinery crude furnace after the 2020 IMO specification change, fouling prediction and a crude diet study delivered a 33% reduction in furnace downtime.