Polymer reactors are among the most demanding equipment in the process industries. Unlike a reactor that makes a single molecular species, a polymer reactor makes a population of chains. Their molecular weight distribution, branching and crosslinking depend on the exact temperature, residence time and catalyst conditions each chain saw as it formed.
A one-degree temperature shift can change chain length disproportionately, and once the polymer is formed no downstream operation can correct it. Nonlinear chemistry, tight quality windows and large exothermic heat loads make polymer reactors a strong case for models learned from plant data.
How reactor type sets polymer properties
Reactor configuration directly determines molecular weight distribution, branching and crosslinking, and once a chain forms under a given set of conditions, those properties are fixed. Each major industrial reactor type creates a different relationship between operating conditions and product quality.
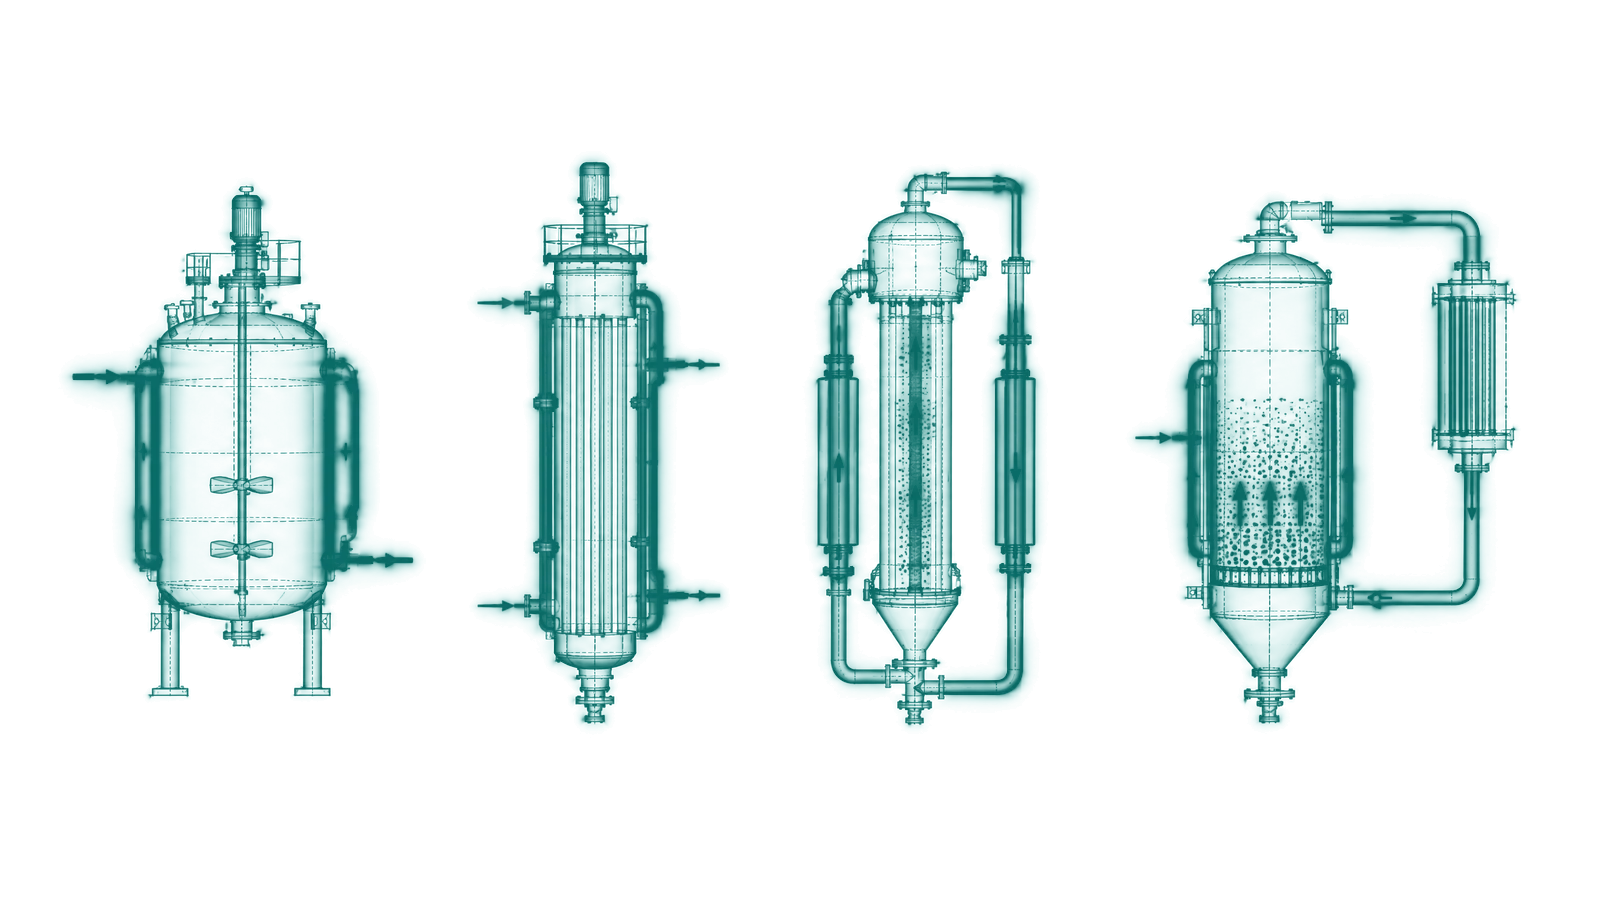
- Continuous stirred tank reactors (CSTRs) give good mixing and temperature uniformity, and they are a common choice for large-volume polyethylene and polypropylene. Their main constraint is viscosity. As conversion rises, high-viscosity polymer mixes increasingly poorly, which often limits practical conversion.
- Tubular (plug flow) reactors offer high conversion and precise control of reaction conditions, but heat removal becomes the dominant constraint as pipe diameter grows. Heat has to travel from the center of the pipe to the cooling jacket at the wall, so the risk of thermal runaway rises with diameter.
- Loop reactors circulate a slurry of catalyst and diluent under pressure through closed piping loops, with heat removed through the loop walls. They are widely used for polyethylene and polypropylene. Their constraint is holding uniform residence time as flow patterns change with polymer concentration.
- Fluidized bed reactors suspend catalyst particles in a gas-phase monomer stream, which avoids the viscosity problem. They are the standard configuration for HDPE and LLDPE. Their constraint is heat removal at the particle level. Particles that cannot transfer energy to the gas fast enough overheat, melt and agglomerate.
The reactor type sets the boundaries for everything that follows: which control strategies are possible, which failure modes are most likely and how tightly quality can be held. It also shapes the model. A CSTR model has to account for mixing that degrades at high viscosity, a tubular reactor model has to follow heat transfer along the pipe, and a fluidized bed model has to represent heat removal at the particle level.
Why polymer reactors are hard to control
Polymer reactors are hard to control because the chemistry is strongly nonlinear and quality feedback takes hours to arrive.
Nonlinear kinetics and exothermic heat loads
Polymerization releases a large amount of heat, often more than simple jacket or coil cooling can remove at commercial scale. In fluidized beds, local overheating can melt particles and form sheets or chunks that disrupt fluidization. In tubular reactors, hot spots can double local reaction rates and set up a runaway feedback loop.
Temperature, chain-transfer agent concentration and catalyst activity interact in ways a linear model cannot represent. A small change in hydrogen feed can shift molecular weight distribution more than operators expect, and the size of that shift depends on the current catalyst state, residence time and temperature profile along the reactor. In a polymer system, the gap between model and reality turns directly into off-spec product.
The lab sampling delay
In many polymer plants, melt flow index and density sample cycles stretch to several hours. During that window a drifting reactor can make large volumes of material under suboptimal conditions, filling silos with product of uncertain quality. Operators compensate by running conservatively, and accept lower throughput as the price of avoiding off-spec penalties.
Grade transitions
Grade transitions amplify both constraints at once. Each changeover takes the reactor through a period where old and new material coexist and quality parameters are moving. A cautious approach stretches the transition to limit risk, and material made during transitions can be a substantial share of total off-spec production.
Where traditional control falls short
PID loops handle single variables in isolation. Advanced process control (APC) manages multiple variables but still assumes roughly linear relationships within a defined operating window. Polymer reactors routinely operate outside both assumptions.
The disturbances also move on different time scales. Catalyst aging shifts the relationship between temperature and molecular weight over weeks, while a change in feed quality can alter reaction kinetics within hours. Fouling lowers heat-transfer coefficients gradually and hides the degradation until it crosses a threshold that forces a shutdown.
These effects interact. A catalyst near the end of its life responds differently to the same feed composition change than a fresh catalyst does, and a linear model cannot anticipate that compound effect.
The result is a control strategy built on conservatism. Operators widen safety margins, accept lower throughput and schedule cleaning on calendar intervals rather than actual equipment condition. Each choice is rational on its own. Together they add up to margin erosion that compounds over months and years.
How learned models address reactor complexity
Models that learn reactor behavior
Rather than relying only on first-principles equations that approximate the kinetics, a data-driven model trains on years of plant history to learn the actual relationships between process variables and product properties. Because it learns from how the specific reactor behaves, it picks up the differences between reactor types without a separate set of generalized equations for each.
Such a model can capture interactions that APC configurations miss: how catalyst age combines with feed quality to shift molecular weight distribution, how fouling changes the relationship between jacket temperature and reactor temperature, and how seasonal cooling-water temperature limits achievable throughput.
A model that keeps learning from new operating data adapts as conditions evolve. Catalyst deactivation, equipment wear and feedstock variability become part of what the model represents. First-principles kinetic models need periodic retuning by specialist engineers to keep up with the same changes.
Real-time quality inference
Inferential models trained on historical sensor readings and the matching lab results fill the sampling gap with continuous quality estimates. When predicted melt flow index starts drifting toward a specification limit, operators or the controller can adjust hydrogen feed, reactor temperature or comonomer ratio before the deviation shows up in the lab.
Quality inference also tightens grade transitions. From historical transition data, the model can find the fastest setpoint sequence between two specifications that keeps product within limits. Shorter transitions add capacity without new equipment, and for plants that run many grades, the time recovered across a year of transitions can become a measurable throughput gain.
What the model needs to start
A polymer plant can begin with the data it already has in its distributed control system (DCS), historian and lab information system. Perfectly structured data is not a prerequisite. The model trains on historical sensor readings, lab results and operating records, and the modeling work itself tends to expose sensor issues, sampling gaps and measurement inconsistencies, so data quality improves in parallel.
Building operator trust
Experienced operators are right to question any system that claims to know their reactor better than they do. No model replaces the pattern recognition that comes from years at the board. Projects that succeed bring operators in from the start and treat them as contributors to the model's development.
Most projects begin in advisory mode. The model recommends setpoint changes and operators keep full decision authority, testing each recommendation against situations they know. When operators see their own decision logic reflected in the model, they start to treat it as their own. Shared recommendations also give every crew the same reference for handling grade transitions. Advisory mode is the step toward closed loop, where the controller writes setpoints to the DCS, inside limits set by plant engineers.
How Imubit applies this
In chemicals and polymers, Imubit applies Map, Model and Control to reactor constraints like these. Map traces off-spec, transition and fouling losses to the recurring decisions behind them. Model uses Deep Learning Process Control® (DLPC®) to learn a nonlinear dynamic model of each reactor from its own history, guided by first principles. Control takes the critical decisions to closed loop, writing setpoints to the existing APC or DCS minute by minute, inside limits set by plant engineers.