Melt flow index (MFI) is one of the fastest quality checks in polymer production, yet the result often arrives late. A lab sample can come back hours after the reactor conditions that produced it have changed. The delay costs most during grade changes, where each hour of uncertainty adds material that may not meet spec and the cost of off-spec production grows the longer a transition runs. That is why more plants pair routine lab testing with inferred quality models that estimate MFI continuously from live process data.
What melt flow index measures
Melt flow index measures how easily a thermoplastic melt flows under standardized conditions. A known weight pushes molten polymer through a precision die, and the result is reported in grams per 10 minutes (g/10 min). The test goes by several names: melt flow rate (MFR) when the result is a mass, melt volume-flow rate (MVR) when it is a volume, and the older term melt index (MI).
The test is simple by design. That makes it useful for routine quality checks, and it limits how much it can say about melt behavior as a whole.
In operations the relationship is usually direct. A high MFI generally corresponds to lower molecular weight and lower melt viscosity. The material flows easily but may give up some mechanical strength. A low MFI points to higher molecular weight, higher viscosity and better performance in demanding applications such as pressure pipe or heavy-duty film.
Using MFI for quality checks
For engineers qualifying incoming resin or verifying production lots, MFI remains one of the fastest checks on batch-to-batch consistency. It is also a practical screen for degradation. An unexpected increase in flow after processing is a common sign that the material has degraded.
Acceptance limits vary by resin family, additives and customer specification, so plants rely on grade-specific baselines rather than a universal threshold.
The trend tells more than the latest number. Plants that read each result alongside quality history, recent operating conditions and known catalyst behavior make better calls than plants that treat MFI as a standalone pass-fail check.
How MFI testing works under ASTM D1238 and ISO 1133
The instrument, an extrusion plastometer, has a heated barrel, a piston, a standardized die and dead weights that apply a controlled load. Under ASTM D1238 and ISO 1133, the polymer melts in the barrel and flows through the die under defined conditions. The result is either a mass flow rate (MFR, in g/10 min) or a volume flow rate (MVR, in cm³/10 min).
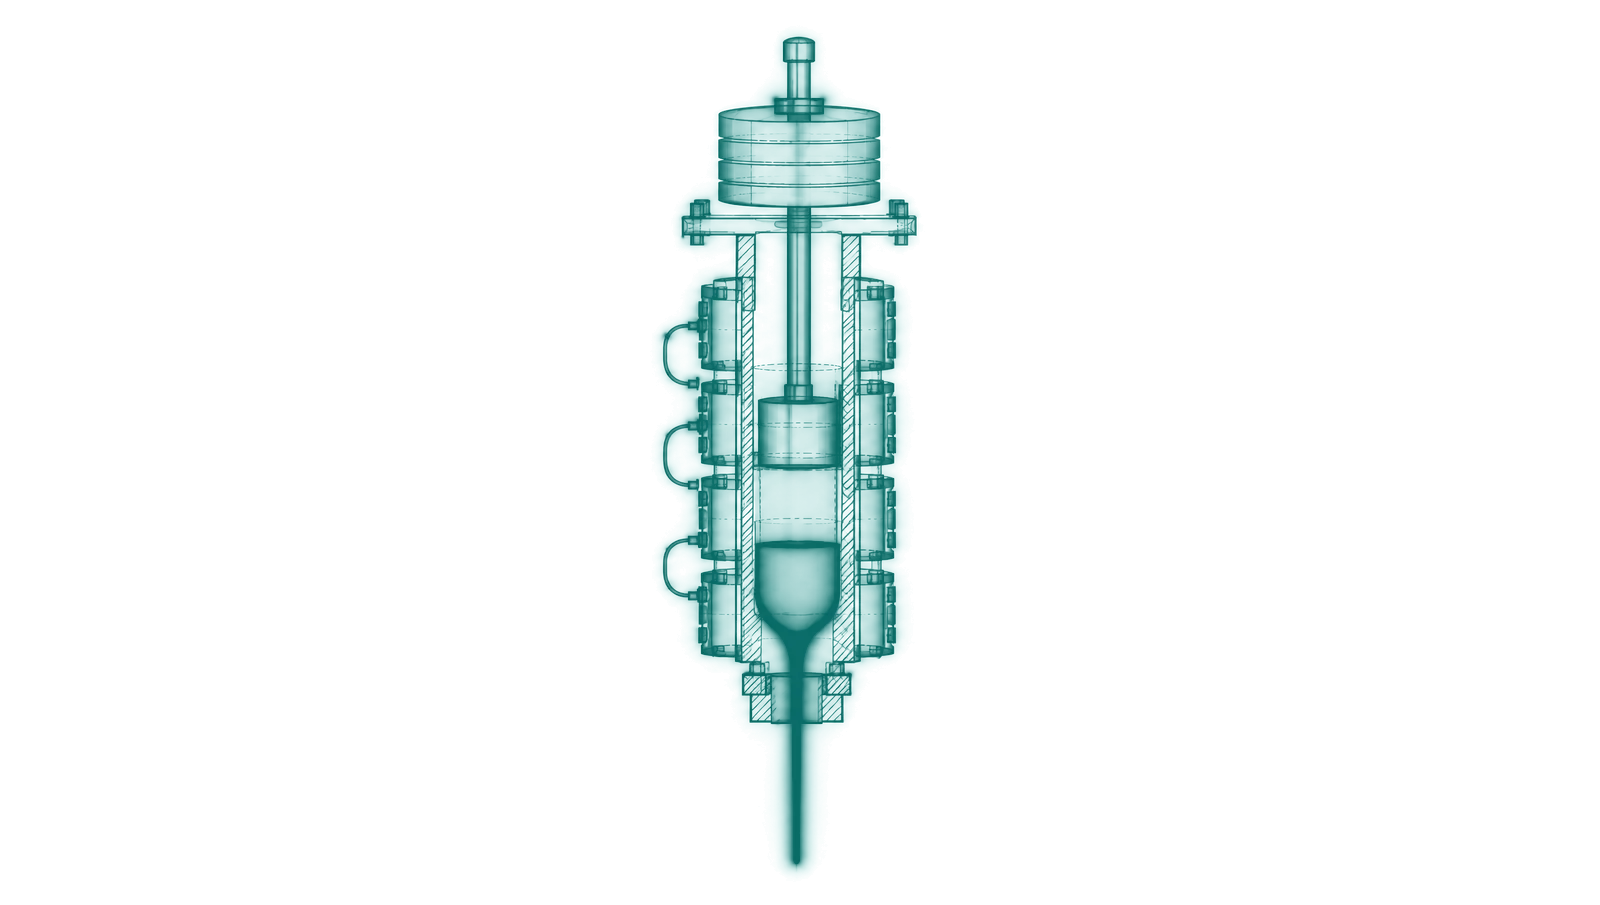
Two procedures dominate production labs:
- Procedure A is manual. The technician cuts and weighs the extrudate at timed intervals.
- Procedure B measures piston displacement automatically and calculates MVR with less handling.
Labs often prefer Procedure B for repeatability, but both depend on disciplined sample preparation and instrument condition.
Standard conditions depend on the polymer. Polyethylene is commonly tested at 190°C with a 2.16 kg load, polypropylene at 230°C with 2.16 kg, and polystyrene at 200°C with 5 kg, each after a defined preheat. Load and temperature strongly affect the result, so values measured under different conditions are not directly comparable.
What affects repeatability
Small handling differences matter more than many labs admit. Moisture, variation in pellet size, incomplete barrel cleaning and inconsistent charge mass can all move the result. The ASTM and ISO methods set the framework. Day-to-day repeatability comes from disciplined execution, reference checks and technique.
Maintenance matters too. Residue buildup and die wear can shift results even when the annual calibration is current. Labs that trend reference materials between calibrations catch drift sooner. Plants that connect lab discipline with reactor operations separate real resin movement from bad test data faster.
Interpreting results across grades and processes
MFI values span a wide range by polymer type and end use. HDPE grades typically fall between 0.1 and 3 g/10 min, with blow molding grades at the lower end. Injection molding HDPE often runs higher, typically 4 to 30 g/10 min, to support faster mold filling. Polypropylene ranges from about 0.5 to 50 g/10 min across the grade spectrum, and specialty meltblown PP for filtration media can be much higher.
The application usually explains the target:
- Injection molding favors moderate to higher MFI so the melt fills the mold quickly.
- Extrusion and film usually need lower MFI, because higher melt strength supports bubble stability and dimensional control.
- Blow molding also trends lower, because the parison has to hold its shape before cooling sets it.
Reading MFI near a grade transition
Interpretation gets harder near grade boundaries. A result inside customer specification may still signal drift if the trend is moving the wrong way and the process is close to a transition cutoff. That matters during reactor grade changes, when the team is deciding whether to keep pushing toward the next target grade or hold longer to protect saleable inventory. Off-spec production in these windows lowers first pass yield, and the cost grows quickly when transitions run long.
The limits of MFI as a single number
Two materials with the same MFI can behave differently in processing if their molecular weight distributions or branching structures differ. The test measures flow at a single, relatively low shear condition, while industrial processing can impose much higher shear rates.
Plants producing several PE or PP grades to tight reactor consistency targets often find that MFI does not explain all the variation they see downstream. This is especially true with recycled feedstock blends, where thermal history shifts flow behavior.
When MFI does not explain what operators see on the line, plants move to broader characterization:
- Capillary rheometry measures viscosity across a range of shear rates.
- Gel permeation chromatography shows the molecular weight distribution.
- Differential scanning calorimetry (DSC) confirms thermal behavior.
The gap may come from resin chemistry, test setup or processing history rather than a single reactor shift.
From lab results to production decisions
The largest return on MFI data comes from shortening the time between measurement and action. While a sample is in the lab, operators adjust based on conditions the unit has already moved past. Narrowing that window pays off most during grade transitions.
Inline measurement and inferred quality models
Plants close the gap in two main ways. Some install inline viscosity measurement to get a more frequent quality signal near the process. Others build soft sensors, inferred quality models that estimate MFI continuously from live process variables such as temperature, pressure, hydrogen ratio and catalyst feed. Both give operators a working quality signal sooner than the lab can.
Lab MFI remains the standard for release testing and lot-to-lot comparison. Inline viscosity and inferred MFI are most useful when response time matters more than certification: during unstable periods, startup recovery and transitions. Used this way, MFI moves from a lagging indicator to something close to a real-time input.
One quality signal for operations, quality and planning
A shared quality model changes how functions work together. Operations can see likely drift while quality is still waiting on lab confirmation. Quality can prioritize sampling and interpretation. Planning can make earlier calls on inventory routing and transition timing with the same view of grade performance. When a change appears, everyone works from the same basis to decide whether it is normal process movement, analyzer bias or a real shift in resin behavior.
During a transition, the inferred MFI trend works as a directional signal rather than a release decision. A rising or falling estimate tells the team whether the unit is moving toward the next target grade before the lab confirms it. Teams combine that signal with process conditions, inventory constraints and the transition logic in their polymer processing strategy.
Building trust in steps
No model captures every instinct behind a veteran operator's judgment. It can preserve the observable relationship between process conditions and quality results across thousands of operating hours.
Many plants start in advisory mode, where the model recommends and operators decide. Newer operators get the same quality signals that experienced operators infer from pattern recognition, which doubles as practical operator training. Experienced operators stay focused on exceptions and edge cases.
Advisory mode is a step on the way. As recommendations prove consistent with plant results, sites move to operator-approved deployment with validated recommendations and operator oversight, and then to closed-loop control, where the model writes setpoints within limits the operators set. For plants already working on real-time optimization, MFI prediction is often one of the most practical early applications, because the cost of waiting for the lab is easy to see.
How Imubit applies this
Imubit applies Map, Model and Control in chemicals and polymers. Map traces off-spec and transition losses to the recurring decisions behind them, such as transition timing and reactor targets. Model uses Deep Learning Process Control® (DLPC®) to learn how reactor conditions drive quality properties such as MFI from the plant's own history, guided by first principles. Control takes those decisions to closed loop, writing setpoints to the existing APC or DCS, inside limits set by plant engineers.