Cement is the binder of modern construction, and the process that makes it is chemically complex, energy-intensive and demanding to operate. Every tonne starts as limestone and ends as a fine powder that has to meet tight specifications, after crushing, blending, high-temperature calcination and finish grinding. According to the IEA cement tracker, the sector's direct CO₂ emissions intensity has stayed broadly flat for about five years, even as regulatory and market pressure has grown.
How cement is made, from limestone to finished product
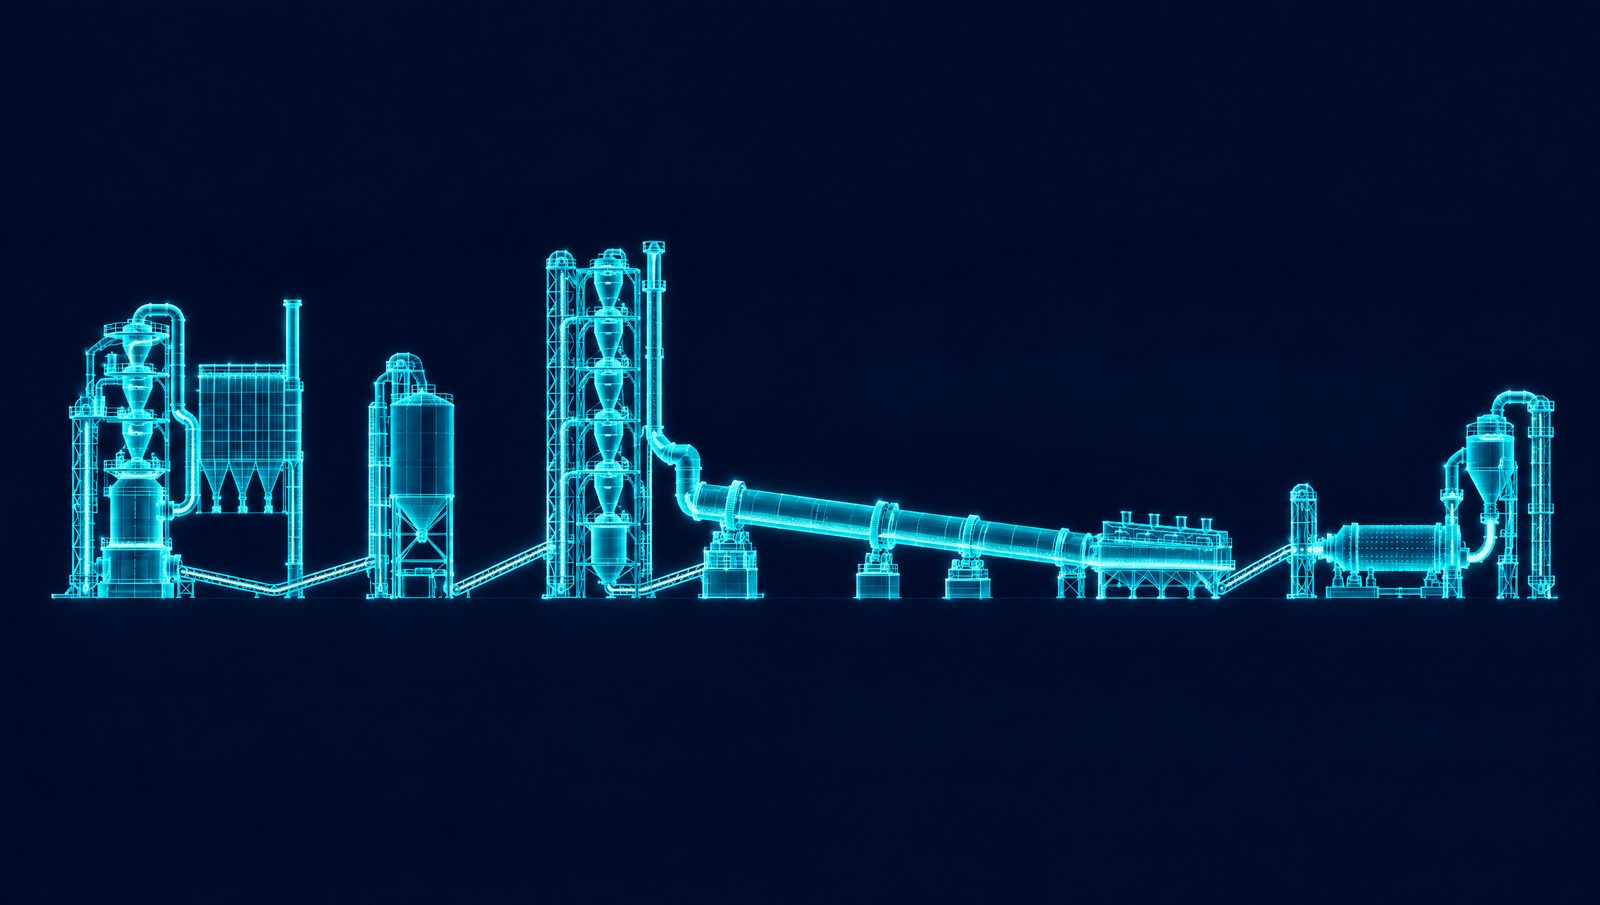
Plants can run wet, semi-dry or dry process configurations. The industry has consolidated around the dry process because its specific energy consumption is substantially lower, and the older processes now survive mostly in legacy plants. Each stage of the dry process brings its own energy, quality and emissions trade-offs.
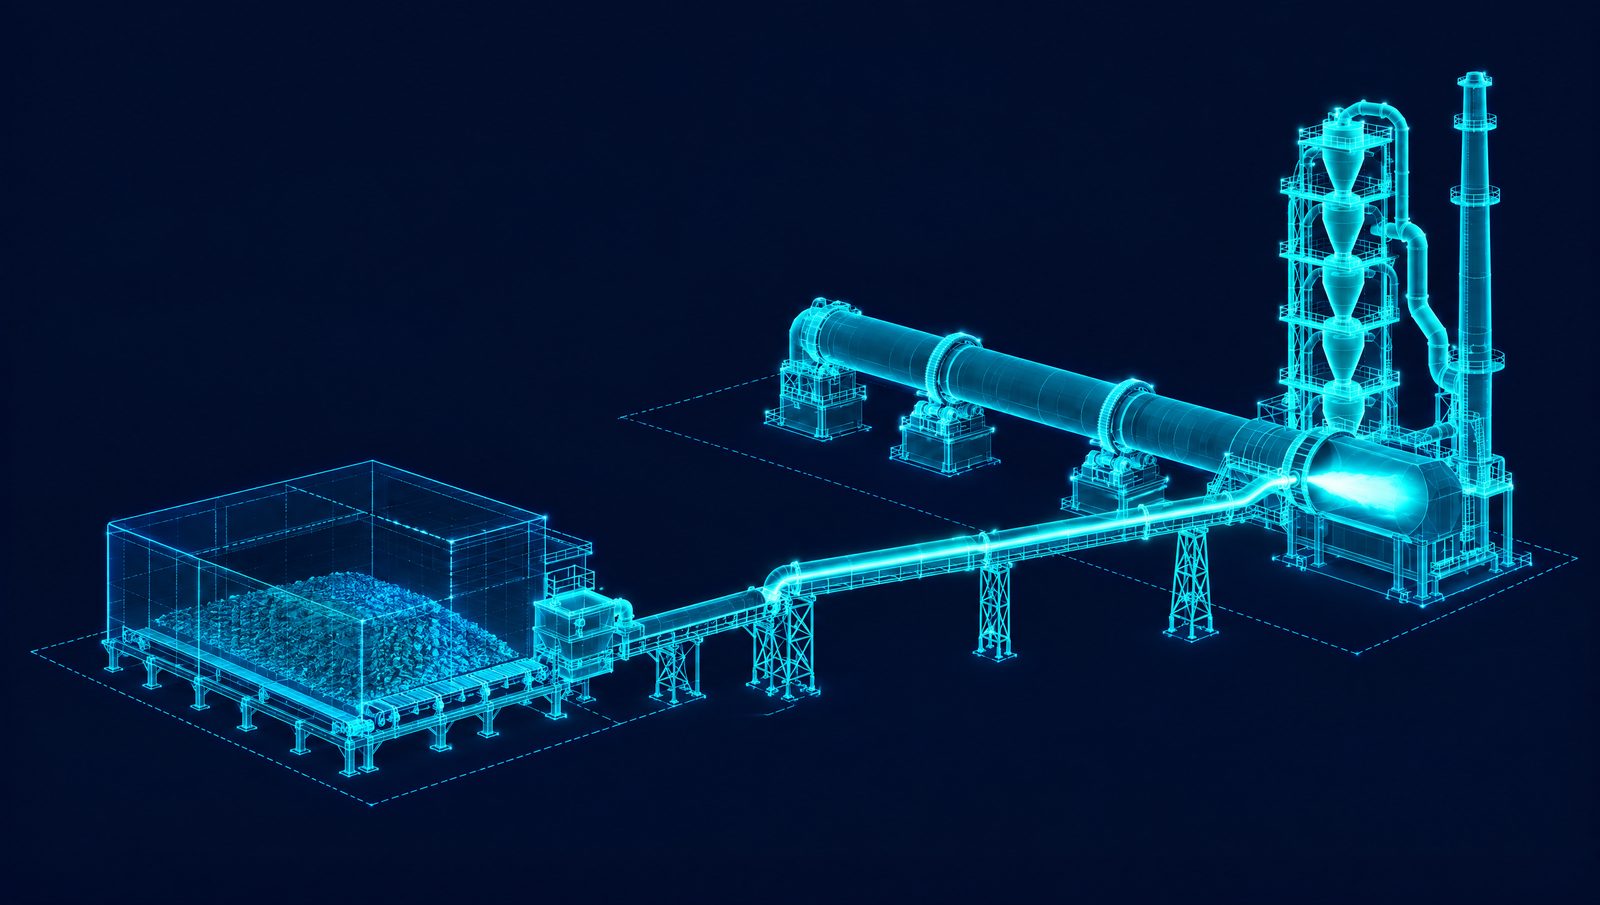
- Raw material extraction and crushing. Limestone, which supplies the calcium, is quarried from surface deposits and transported to the plant. It is blended with clay or shale for silica and alumina, iron ore for iron oxide, and sometimes fly ash or bauxite. Primary and secondary crushers reduce these materials to a size the mills can handle.
- Raw meal blending and grinding. The crushed materials are proportioned, blended and ground into a fine powder called raw meal. Its chemistry sets clinker quality, so analyzers and blending silos work together to hold the target composition as the quarry face varies.
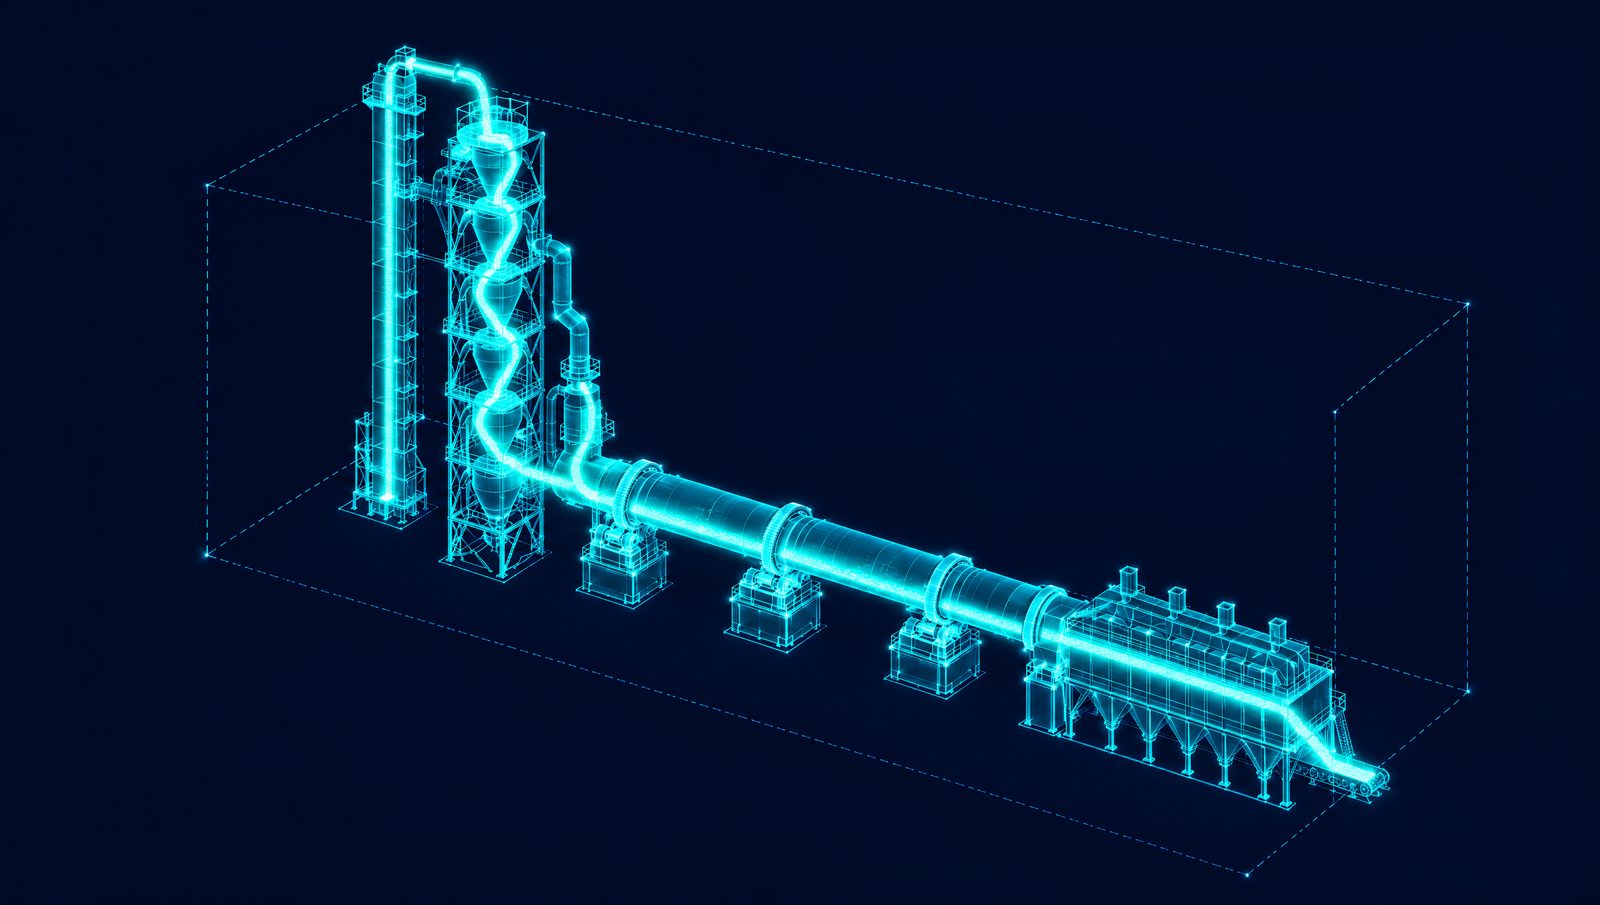
- Preheating and calcination. Raw meal passes down a cyclone preheater tower, where hot kiln gases drive off moisture and start calcining the limestone. In the calciner, calcium carbonate decomposes into calcium oxide and CO₂, which releases most of the process emissions associated with cement.
- Kiln and clinker formation. The preheated meal enters the rotary kiln, where the material reaches about 1,450°C in the burning zone. At that temperature it sinters into clinker nodules, the mineral phases that give cement its binding properties. Fuel, air flow and feed rate have to stay balanced to keep free lime within specification.
- Clinker cooling. The clinker cooler drops the clinker temperature quickly to lock in the mineral structure formed in the kiln, and recovers heat that returns to the kiln and calciner as combustion air.
- Finish grinding and packaging. Cooled clinker is ground with gypsum in cement mills to a specified fineness, measured as Blaine specific surface area. For most plants the product is Portland cement, stored in silos and dispatched in bulk or in bags.
Each stage depends on the one before it, so variability upstream tends to grow as it moves through the process. The process choice also shapes a plant's energy efficiency long after commissioning. That is one reason further efficiency gains in the sector now depend less on new equipment and more on how well plants operate the equipment they have. For the process economics in more detail, see the cement manufacturing process.
The constraints shaping modern cement plants
Modern plants operate under overlapping pressure from emissions regulation, energy cost, quality consistency and workforce change. Each one shows up as an operating constraint in the control room.
Emissions chemistry and fuel variability
Calcination releases the majority of a cement plant's direct CO₂ emissions, and fuel combustion contributes most of the rest. That chemistry cannot be avoided, but every kilogram of off-spec clinker and every degree of unnecessary firing adds to the footprint. Plants working toward decarbonization targets have to tighten operation inside a process that resists tight control.
Alternative fuels add variability. Tire-derived fuel, biomass and industrial waste substitute for coal and petcoke and reduce emissions and fuel cost, but their composition shifts from batch to batch. Calorific value, moisture, and chlorine or sulfur content can all move with the feed, and each changes how the flame behaves in the kiln. A control strategy calibrated for one fuel mix degrades as the mix changes. For how producers discussed alternative fuels at the 2025 IEEE-IAS/PCA Cement Conference, see AI, AFR and 1L.
Lab delay on free lime
Free lime is calcium oxide that did not combine during clinker formation, and it is the key indicator of clinker quality. Too much free lime signals incomplete reactions and can cause unsoundness in the finished cement. Too little signals overburning, which wastes fuel and shortens refractory life.
The measurement comes from the lab, hours after the clinker leaves the kiln. Operators compensate by holding the kiln hotter than conditions require, protecting quality they cannot verify in the moment. That buffer costs fuel, adds thermal load on the refractory lining, and limits how hard the kiln can be pushed when feed rate or fuel economics would justify it.
Workforce change at the control board
Experienced control room operators and process engineers are retiring faster than plants can replace them, and the pattern recognition built over decades on one kiln does not transfer easily to new hires. Training a new operator to competency at the board typically takes years, and the simulators available rarely capture the quirks of a specific kiln.
In the meantime, free lime stability and Blaine targets depend on whoever is on shift. That widens the performance gap between crews and makes any push to tighten operation harder.
Why traditional APC falls short
Traditional advanced process control (APC) was designed for processes where measurements are reliable and inputs are stable. Kilns rarely offer either. Raw material chemistry shifts between quarry faces, alternative fuel composition moves continuously, and APC models drift away from the conditions they were tuned for. Control Global reports that about 65% of APC projects are turned off in their second or third year when regular recalibration is not scheduled.
How AI addresses these constraints
AI models learn from the plant's own operating history, which matters in a process where direct measurement is limited and conditions keep changing. Plant-specific models do not depend solely on first-principles equations tuned to idealized conditions. They capture the relationships between process states and the actions that produced good outcomes.
A tighter free lime feedback loop
With lab results lagging by hours, a model that infers free lime from real-time process variables gives operators a continuous estimate between lab samples. That can reduce the extra firing many plants hold as a quality buffer, so fuel use falls without loosening specifications. See free lime prediction for real-time control.
Adapting to fuel and grinding variability
Models trained on a broad operating history respond to fuel composition shifts because they reflect how the plant behaves across conditions, beyond the snapshot taken at commissioning. That supports more stable clinker quality, and variability downstream falls in turn. The same models support steadier pyroprocessing as the fuel feed changes.
Optimizing across the plant extends the benefit beyond the kiln. Steadier grinding circuits hold Blaine fineness targets with less energy per tonne, so stability upstream becomes measurable savings downstream. See cement grinding optimization.
A supervisory layer above existing controls
The optimization layer sits above the existing controls in a supervisory role and leaves them in place. It communicates through standard protocols such as OPC UA and writes recommendations or setpoints to the existing distributed control system (DCS). Plants can tighten control without rebuilding the infrastructure that already runs the process.
Building trust in advisory mode
Deployments usually begin in advisory mode. The model recommends setpoints and operators decide whether to apply them. The recommendations appear on the screens operators already use, and the reasoning behind each one can be traced to the process conditions that shaped it.
This stage does more than lower risk. Operators can compare recommendations with live conditions, judge whether the model reads the unit correctly, and see strategies shaped by the plant's history as well as by whoever is on shift. As the model proves itself, the plant moves to closed loop with operators able to take over at any time.
Advisory mode and workforce continuity
The advisory stage also shortens ramp time for new operators. Instead of depending entirely on years beside a veteran at the board, new hires can watch the model's recommendations develop in real time and compare them with their own reasoning. The model that supports optimization doubles as a training tool, which narrows the knowledge-transfer gap as the workforce changes.
No model matches the instincts a veteran builds over years on the same unit. A model can still hold the observable relationships between process states and the actions that produced good results, and keep them available across shifts, fuel conditions and raw material regimes. Coordination improves as well when maintenance, operations and planning work from the same model of plant behavior instead of separate assumptions.
How the Imubit Platform applies
In cement, Map traces the gap between the plan and the plant to the recurring kiln and mill decisions behind it, such as burning zone temperature, fuel mix and separator settings held conservatively against the lab cycle. Model learns the kiln's nonlinear dynamics from its own history with Deep Learning Process Control® (DLPC®), including free lime predictions ahead of the lab. Control takes those decisions to closed loop on top of the existing APC and DCS, with operators able to take over at any time. On a kiln pyroprocess running in closed loop, this approach has delivered a 20 to 30% reduction in process variability.