Pyrolysis gasoline, or pygas, is the naphtha-range, aromatics-rich liquid byproduct of steam cracking. It can be blended into the gasoline pool for its octane, or routed to BTX extraction to recover benzene, toluene and xylenes. For an olefins complex, that routing choice carries real margin.
With the chemical sector facing overcapacity and soft demand, producers are looking for more value from the assets they already run, and pygas is one of the places to find it. Raw pygas is unstable, its composition shifts with cracker economics, and selective hydrogenation performance shapes every recovery option downstream. Most of the recoverable margin depends on getting feedstock choice, hydrogenation severity and product routing right. Keeping hydrogenation severity and routing aligned as feed conditions move is one of the more consequential levers in olefins plant operations.
What drives pygas composition and value
Pygas forms when a steam cracker breaks down heavier hydrocarbons to make ethylene and propylene. It spans C5 to C12 and contains aromatics (mainly benzene, toluene and xylenes), olefins, diolefins, styrenics and paraffins. Its high octane supports direct blending into finished gasoline, and its high aromatics content makes it a valuable feed for BTX extraction, mainly for benzene and to a lesser extent toluene.
Cracker feed sets the composition ceiling
Pygas composition follows cracker feed, and that composition sets the ceiling on what downstream processing can recover. The diolefins, styrenics and reactive olefins in fresh cracker liquid polymerize and form gums if they are not stabilized, so selective hydrogenation normally follows directly after the quench. Beyond stabilization, the aromatics share decides whether BTX extraction is economic at all.
Naphtha-fed crackers produce pygas with substantial BTX. Chemical Engineering reports steam cracker gasoline BTX content of around 56 to 80 wt%. Ethane crackers produce a few percent pygas by yield, with a different aromatics profile.
Heavier feeds yield more liquid co-products per unit of cracker throughput. Lighter feeds favor ethylene selectivity at the expense of pygas volume. Benzene usually carries most of the recoverable value, because recovering mixed xylenes from pygas is often uneconomic given typical xylene content and high ethylbenzene levels.
Feed transitions disturb downstream units
When a cracker shifts from naphtha to LPG for ethylene margin, pygas throughput drops. What remains arrives with a different diolefin content, sulfur speciation and carbon number distribution. The pygas hydrogenation unit has to reoptimize around a composition disturbance it did not cause and cannot predict from its own instruments. The response spans first-stage severity, hydrogen allocation and fractionation targets. Managing those handoffs is one of the harder parts of running an integrated olefins complex.
How two-stage hydrogenation shapes processing routes
The pygas upgrading train has three sections. First-stage hydrogenation stabilizes the reactive stream. Second-stage hydrogenation removes the remaining olefins and sulfur. Fractionation splits the stabilized product into recoverable cuts. How those sections run sets the margin available at every route choice that follows.
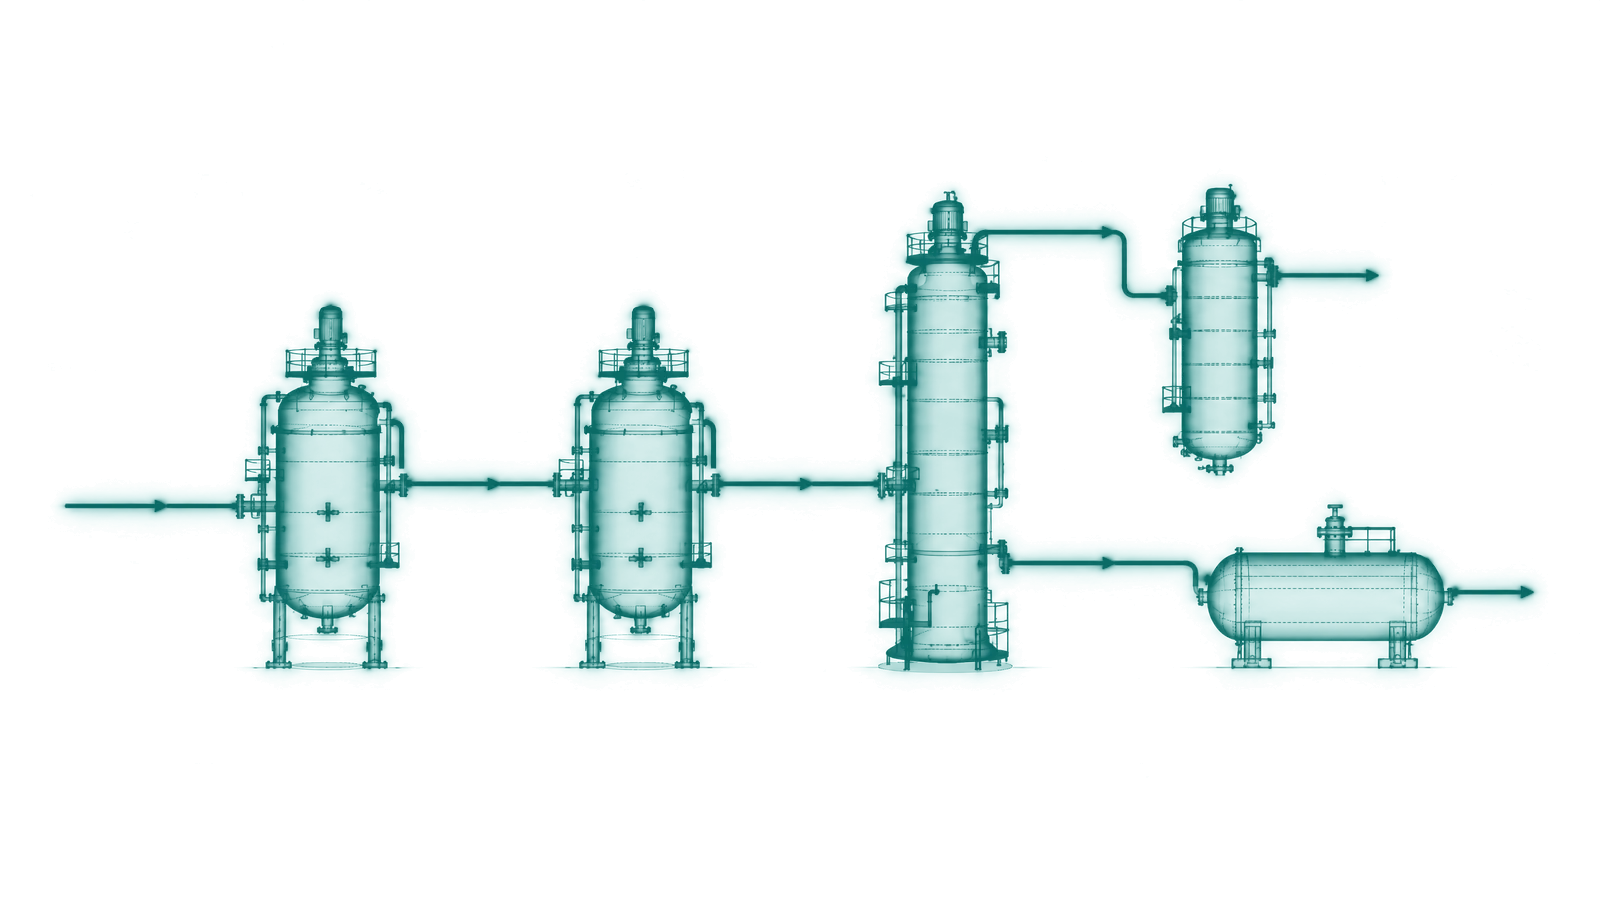
First-stage hydrogenation (GHU-1)
GHU-1 selectively converts diolefins, styrene and some olefins in liquid-phase fixed-bed reactors. It has to stabilize the stream without saturating the aromatics that carry the product value, and that sets the operating window for everything downstream.
Incomplete conversion in GHU-1 degrades every section after it. Residual diolefins carry into GHU-2 and the extraction equipment, where they contribute to gum formation and fouling on reactor beds, exchangers and column internals. Undersized or poorly run hydrogenation pulls down first-pass yield across the whole train.
Second-stage hydrogenation (GHU-2)
GHU-2 completes olefin removal and hydrodesulfurization of the C6 to C8 heart cut. Its core constraint is selectivity. Sulfur and olefin conversion have to be pushed while aromatic ring saturation stays near zero.
Both reactions release heat in the reactor bed in similar ways, so temperature measurement alone cannot cleanly separate them. That makes reactor selectivity harder to hold with single-loop control.
Choosing a processing route
After hydrogenation, sites choose among several routes:
- BTX extraction recovers benzene, toluene and xylenes from the C6 to C8 cut.
- Styrene recovery takes styrene out before full hydrogenation, where market economics support the extra processing.
- Thermal hydrodealkylation converts toluene into more benzene.
- Aromatics saturation prepares the stream for recycle to the cracker, when olefin value is stronger than aromatics value.
- Gasoline blending captures octane value but leaves chemical value unrecovered.
Benzene limits in finished gasoline also cap how much raw pygas can be blended. Extracting benzene first can increase the remaining stream's blending flexibility while lifting product value.
C5 fractions add value at the margin, but recovery economics depend on site scale and available infrastructure. The same applies to deeper recovery beyond benzene and toluene. In practice, route selection is an ongoing chemical process optimization problem, shaped by live spreads between benzene, styrene, isoprene and ethylene, and by feed quality and unit constraints.
Where conventional pygas control loses margin
Pygas units run under coupled constraints that conventional control handles poorly. The failure modes that cost the most involve catalyst poisoning, selectivity loss and coordination gaps between units and teams.
Catalyst poisoning and cycle-length loss
A common failure mode is poisoning by sulfur species carried over from the cracker. Elevated CS₂ in particular is known to deactivate palladium-based GHU-1 catalysts. Cycle length shortens, and operators raise reactor inlet temperature to compensate.
Higher temperature then accelerates coke deposition, which shortens the cycle further and raises energy cost. Managing that temperature escalation is a real margin lever, but it depends on knowing the catalyst's activity, which has to be inferred from conversion and pressure-drop signatures because it cannot be measured directly.
The coordination gap in single-loop control
Single-loop PID control handles each variable on its own. It cannot coordinate hydrogen-to-feed ratio, reactor temperature profile and space velocity across two interdependent reactor stages with competing conversion targets. Tuning a cascade of setpoint controllers to hold both GHU-1 and GHU-2 at their selectivity limits while feed composition drifts is a job single-loop control was not designed for.
Separate teams, separate views
The problem is also organizational. Maintenance tracks catalyst condition, operations manages reactor setpoints, and planning decides product routing from market prices. When those groups work from separate data and separate models, the integrated optimum is hard to see. Good historian practice helps, but it takes a shared dynamic model to put catalyst state, conversion and margin in front of all three groups at the same time.
What a learned model changes
Advanced control has been applied to pygas hydrogenation for years and can improve performance. Models identified on one feed slate, though, can misrepresent the process as conditions drift, and keeping them current is an ongoing burden on many sites.
A model learned from the unit's own operating history, across many feed slates and catalyst cycles, captures interactions that are hard to see from the board: how GHU-1 severity, the GHU-2 temperature profile and extraction feed quality affect one another. Models that have learned from past feed transitions can anticipate the setpoint shifts that follow a feed change, instead of waiting for conversion to deviate downstream. Operator judgment built over years at the board still decides which recommendations to act on.
Several improvements need no new equipment:
- Tighter reactor temperature control can extend catalyst run length.
- Better coordination between hydrogen allocation and reactor severity can reduce both over-hydrogenation of aromatics and under-conversion of olefins.
- Routing decisions tied to current benzene and gasoline spreads can recover more value from existing infrastructure.
Starting in advisory mode
Plants usually start in advisory mode. The model recommends setpoint changes and operators decide whether to accept them. Operators keep full authority while confidence builds, and the model is useful from the start in several ways:
- Operator training on real transitions. Newer operators can practice feed-switch and catalyst-aging scenarios offline, on a simulation built from the plant's own history.
- What-if evaluation before each move. When feed quality drops or a downstream slate shifts, operations can see the predicted effect on GHU-2 selectivity, extraction yield and finished benzene quality before committing to a change.
- Consistency across shifts. Every shift works from the same recommended operating point, which reduces the variability that appears when different crews run the same unit from different mental models.
- Planning and economics. The same model can test pygas routing against current benzene and gasoline spreads, informing whether to push BTX extraction or blend more into the pool.
As the recommendations hold up through feed transitions and catalyst aging, the next step is closed loop. The controller writes setpoints to the APC or DCS, and operators can take over, within the limits they set.
How the Imubit Platform applies
On chemical and polymer plants, the Imubit Platform applies Map, Model and Control to the pygas train. Map traces lost benzene recovery and shortened catalyst cycles to the recurring decisions behind them, such as GHU-1 severity, hydrogen allocation and product routing. Model uses Deep Learning Process Control® (DLPC®) to learn the catalyst and feed-composition behavior of both reactor stages from the unit's own history. Control takes those decisions to closed loop, inside limits set by plant engineers, writing setpoints to the APC and DCS already in place.