Compressor surge is an unstable flow condition in which gas momentarily reverses through a centrifugal or axial compressor. The resulting pressure oscillations hammer impellers, bearings and seals, and the damage can develop in milliseconds. The cost goes well beyond the repair bill. Unplanned downtime on a compressor can disrupt production across a whole process unit, and plant reliability data often singles out compression services.
Surge control protects both the equipment and the operating margin. For many compression services, the open question is whether today's anti-surge strategy is more conservative than current conditions require.
What causes compressor surge
Surge happens when flow drops below the minimum the machine can sustain at the prevailing pressure ratio. Most plants face a combination of triggers rather than a single root cause.
Process-side disturbances
These are the most common starting point. Lower downstream demand, higher system resistance from a partly closed valve or a piping restriction, or a rapid change in upstream supply can each push the operating point left along the compressor curve toward the surge line. A blocked discharge or the sudden trip of a downstream consumer can move flow into the surge region within seconds.
Mechanical degradation
Wear and fouling act slowly but persistently. Impeller wear, diffuser fouling and seal leakage shift the compressor's performance map over weeks and months. The surge line moves as the machine's health changes, and the margin set at commissioning erodes with it.
Shifts in operating conditions
Variable feed makes these the hardest to manage. Higher inlet temperature lowers gas density and shifts the surge boundary on the compressor map. Changes in molecular weight from feed variability or liquid carryover alter the compressor's aerodynamic capability in ways a fixed surge control line cannot follow. A recycle gas compressor handling variable feed faces a surge boundary that moves with every change in gas composition.
Speed-related triggers
These act fastest. When the performance controller that manages speed runs without coordination with the anti-surge controller, the two can drive the operating point back and forth near the surge line. The risk peaks during transients, when several control loops have to stay aligned.
How to detect surge before damage occurs
Reliable detection combines thermodynamic and mechanical signals. Each signal type sees a different part of the phenomenon, and each has blind spots when used alone.
Flow
Flow responds fastest. Swings in suction flow between surge peaks and valleys appear in flow measurements before pressure measurements register them, because suction and header volumes smooth the pressure signal. Even so, a mono-point system that relies on orifice flow alone can still report adequate flow after the operating point has crossed the surge boundary.
Pressure
Pressure picks up the larger oscillations once they develop. The rate of change of discharge pressure is a useful confirming signal, especially for telling a true surge event from process noise.
Vibration
Vibration detects rotating stall, a precursor that shows up as rising sub-synchronous frequencies before full surge develops. Stall is a local flow disturbance in the impeller or diffuser, while surge is a global flow reversal across the whole machine. Vibration cannot be the sole detection method, because some surge events produce no precursor at all.
Combined signals
A reliable architecture combines suction temperature, suction pressure, flow, discharge pressure, discharge temperature, vibration and speed. Design choices for this kind of advanced process control need to accommodate several signal types from the start. Plants that combine these signals dynamically tend to see drift earlier than plants that rely on fixed limit lines.
Anti-surge control and its limits
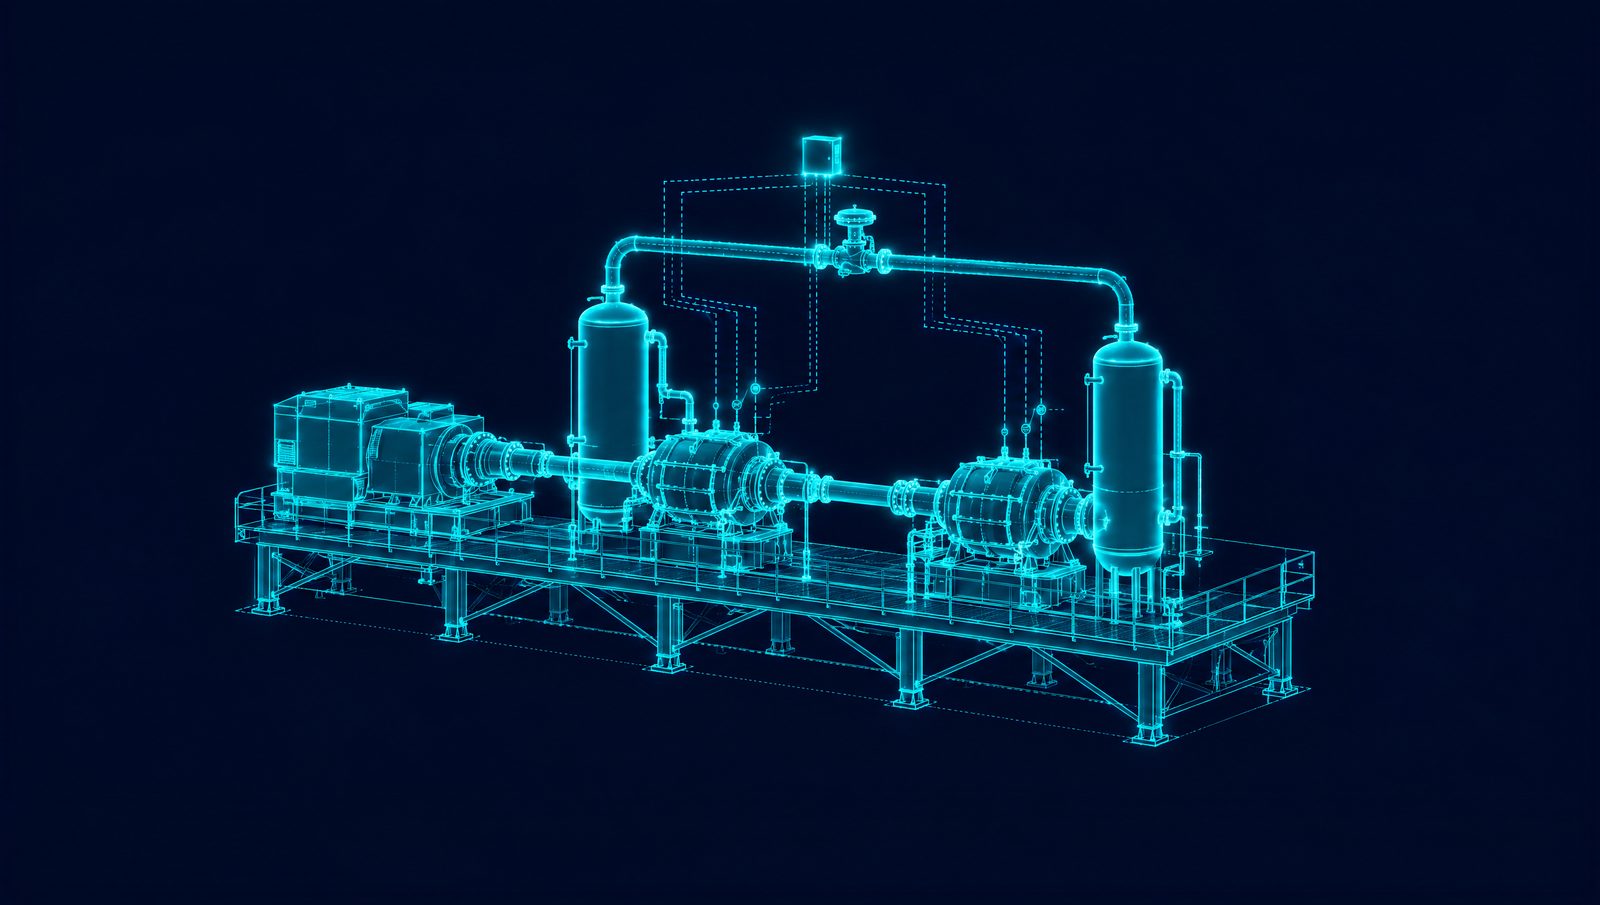
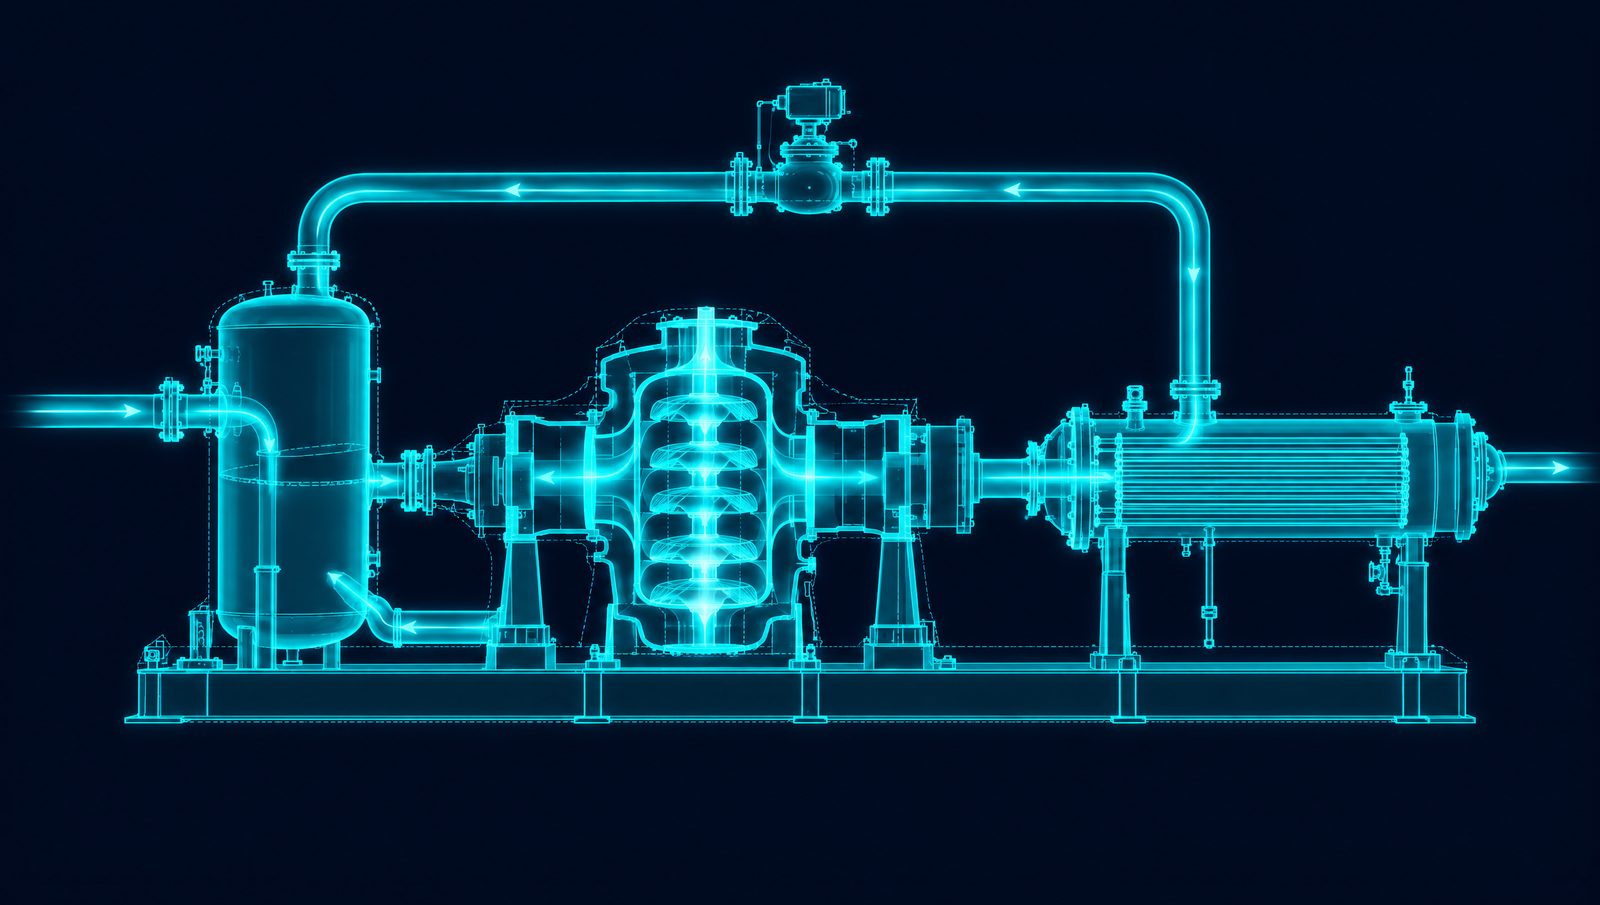
Anti-surge control keeps flow above the safe minimum by opening a recycle valve that routes discharge gas back to suction. The added flow through the compressor moves the operating point away from the surge line and restores stability.
Most anti-surge systems define a surge control line offset from the surge limit line by a margin set at commissioning. When the operating point approaches the control line, the controller modulates the recycle valve to hold the offset.
The architecture works, but it assumes the boundary is a permanent feature of the compressor map. In practice the surge line shifts with inlet temperature, gas molecular weight, fouling and speed, so a control line set at commissioning slowly loses accuracy as the real boundary moves.
Anti-surge valve response time also limits how tight the margin can be. According to Plant Engineering, surge margin design varies widely: a poorly designed system may need a margin of 16% or more, while a well-designed system can operate with margins below 8%. Faster valves and well-tuned controllers allow narrower margins. Slower valves force conservative offsets, so that the recycle opens before the operating point crosses the boundary. Pattern recognition on control system data can complement the dedicated anti-surge controller, which keeps its protection role.
The cost of conservative surge margins
When the anti-surge valve opens, compressed gas returns to suction. Every unit of recycle flow is work already done and then thrown away. The compressor recompresses the returned gas and consumes driver power without delivering net throughput.
A conservative margin is a defensible operating strategy, but its cost is real. The compressor routinely recycles more flow than the instantaneous process state requires, even when current conditions would safely allow a tighter margin.
The energy penalty builds up over operating hours. A minimum flow controller configured for worst-case conditions limits turndown and wastes driver power through normal operation. Gains in industrial energy efficiency show up in kilowatt-hours accumulated over weeks, rather than in any single shift.
In multi-compressor configurations, running machines at equal flow rather than at equal distance from their own surge control lines can push one machine into unnecessary recycle while the others run inefficiently. Lost throughput often appears as an opportunity cost on the production side rather than a line on the energy bill. The gap between what is safe and what is set can widen for months as fouling builds and feed conditions drift, and fixed control logic will not register the change.
Adaptive control that tracks the real surge boundary
Adaptive control treats the surge boundary as a moving target and updates its estimate from operating data. The control system then no longer has to default to worst-case margins.
As fouling accumulates, gas composition shifts and ambient conditions change, the estimated boundary follows the compressor's actual behavior. The effective margin reflects current conditions instead of commissioning assumptions.
Pattern recognition across process and equipment data can identify surge precursors earlier than threshold-based detection. Instead of waiting for the operating point to approach a static control line, the model recognizes multivariable operating patterns and anomaly signatures. Operators get more lead time for corrective action and depend less on emergency valve response.
In multi-train configurations, coordinated control can distribute load so that each machine stays in its most efficient operating region while its individual surge margin holds.
A shared model also changes how teams work together. When maintenance, operations and planning work from the same picture of compressor loading trade-offs, their decisions tend to hold up better than ones made in isolation:
- Maintenance can see how a deferred bearing inspection shows up as less margin headroom.
- Operations can recognize when feed changes tighten surge constraints downstream.
- Planning can set LP targets on what the compressor delivers today, rather than on commissioning assumptions.
Layering control to build operator trust
A sound architecture layers the optimization above the existing anti-surge system. Dedicated anti-surge controllers are built for fast compressor protection and keep that job. The supervisory model adapts the control strategy over time, while the dedicated controller continues to execute real-time protection.
Plants usually start in advisory mode, using the historian and DCS data they already collect from the compressor and the surrounding process. The model learns from that history how the surge boundary moves under varying conditions and recommends setpoint adjustments, which operators evaluate against current conditions and their own experience. Even in advisory mode, the model can improve consistency across shifts, support what-if evaluation when throughput, energy and protection margin conflict, and show gradual degradation as fouling and feed changes alter the compressor's behavior.
As confidence builds, teams validate the recommendations in operation, as a well-run pilot does, and then move to closed-loop setpoint adjustment at a pace operators are comfortable with. This follows the wider move toward human and AI collaboration in plant operations, where the model tracks thousands of variable interactions and operators keep judgment over the trade-offs no model can settle alone.
How Imubit applies this
Imubit's Map, Model and Control approach, described on the platform overview, applies to compressors as part of the process units they serve. Map traces wasted recycle and lost throughput to the recurring decisions behind them, such as surge margin and load-sharing targets. Model uses Deep Learning Process Control® (DLPC®) to learn how the compressor behaves within its process from the plant's own history, guided by first principles. Control writes setpoints to the existing APC or DCS minute by minute, inside limits set by plant engineers, above the dedicated anti-surge controller, which keeps its protection role.