Molecular sieve dehydration units rarely come up in operations meetings, and they get less attention than their effect on train economics deserves. Upstream of liquefaction, regenerable zeolite beds cycle between adsorption and thermal regeneration to take feed gas water below 0.1 ppmv and protect the cryogenic equipment downstream. When a bed degrades faster than expected, or water breaks through, the consequences follow quickly: ice in the heat exchangers, unplanned shutdowns and production lost for days.
Aging beds, fixed cycle timers and upstream contamination shorten dehydration life and limit train throughput. Treating regeneration as a condition-based decision changes those economics.
How bed design shapes lifecycle performance
Design choices made years before commissioning set what the sieve can deliver after sustained cycling. The water specification for LNG feed gas, below 0.1 ppmv, is far tighter than pipeline gas specifications because cryogenic heat exchangers cannot tolerate water slip. Holding that threshold for the full design life is a sizing problem first and an operating problem second.
Type 4A molecular sieve is the standard adsorbent for LNG dehydration. It offers higher water uptake than smaller-pore alternatives, though its larger pore size also adsorbs some CO₂ along with the water. That coadsorption matters because the regeneration gas returns upstream to the gas processing and treating systems. CO₂ carried back into the acid gas removal loop disturbs the units ahead of dehydration.
A 2+1 vessel configuration, with two beds in adsorption while one regenerates, is a common arrangement in LNG trains. It preserves operating flexibility as performance degrades. If one bed underperforms, the train can often continue at reduced throughput rather than stop.
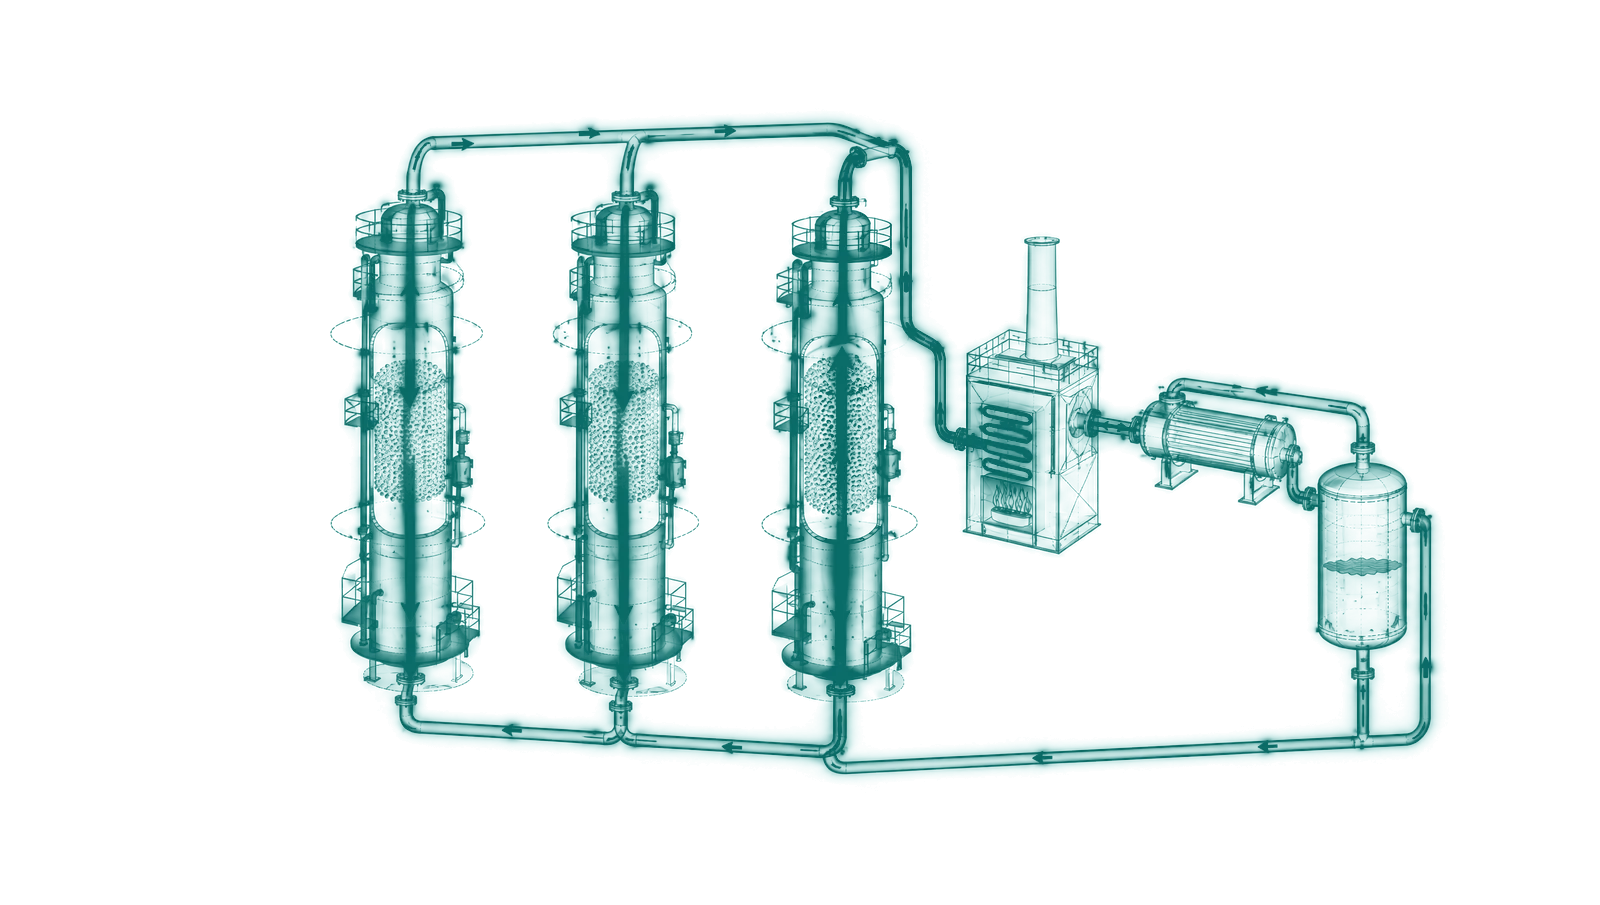
The more important sizing question comes later in the bed's life. A vessel that meets specification at startup but cannot hold 0.1 ppmv after sustained cycling becomes a throughput constraint long before it fails mechanically. The stronger sizing basis is end-of-life performance rather than commissioning capacity. Tracking pressure drop, breakthrough timing and capacity decline against historian records supports that lifecycle view and shows slow drift that single-cycle inspections miss.
How regeneration practice drives bed degradation
Every heating cycle adds thermal stress, and fixed-timer regeneration tends to spend capacity the bed could still use. The temperature swing adsorption sequence moves through heating, cooling and standby before the bed returns to adsorption service. In a 2+1 configuration with adsorption cycles of 12 to 16 hours, the full regeneration sequence has to fit inside the remaining cycle window. That timing pressure is part of why conservative operating habits persist.
Heating and standby
Heating is the most controllable part of the sequence. Excessive ramp rates raise thermal stress and the risk of retrocondensation, where water condenses again inside the bed during heating and erodes capacity. Many LNG units add an intermediate heating hold that gives water time to evaporate before the bed reaches full temperature, which reduces hydrothermal damage to the adsorbent.
Standby matters for a different reason. As the bed ages and capacity declines, breakthrough arrives sooner. In fixed-cycle systems, standby time absorbs some of that shortening. That delays any change to cycle timing, but it uses up margin that could be put to work elsewhere.
Energy use and contamination
Regeneration is the dehydration unit's largest standing energy demand. Regenerating on a fixed timer rather than on current bed condition often spends fuel and thermal life before the bed needs the cycle, and that loss compounds with physical degradation.
Thermal cycling wears the sieve, but field experience consistently points to upstream contamination and carryover as the larger driver of capacity loss:
- Liquid carryover from the upstream treating unit can damage the clay binder, generate fines and raise pressure drop.
- Heavy hydrocarbon fouling blocks pore access. It shows up as reduced adsorption capacity and a longer mass transfer zone, both of which bring breakthrough sooner.
Managed together, regeneration and feed-side discipline behave more like an advanced process control problem than a fixed-schedule routine.
Signs a bed needs replacement before the turnaround
The earliest signs are performance changes rather than mechanical failure:
- earlier breakthrough
- rising outlet water content near the end of adsorption service
- pressure drop climbing faster than the commissioning baseline
- inspection findings such as darkened pellets or hydrocarbon-soaked material
Tracked against cumulative cycle count, these indicators support planning against thermal fatigue and show the trend months before the turnaround window opens.
Condition-based switching in place of fixed timers
Most molecular sieve units still regenerate on a fixed schedule, and that reflects a measurement constraint as much as a control philosophy. Inline moisture analyzers at trace water levels have well-known limitations. Water breakthrough into cryogenic equipment can trigger process safety events with consequences far larger than the cost of conservative cycling. Without a reliable real-time signal of bed loading, operators default to timers calibrated against worst-case conditions. That protects the unit, but it spends fuel and thermal life earlier than the bed needs.
Soft sensors built from existing distributed control system (DCS) process variables can estimate current bed loading without depending on a single direct moisture measurement. The same models can track cycle count, thermal stress history and contamination events, which supports forward planning as well as immediate switching. Cycle timing becomes a setpoint decision driven by bed condition.
Variable cycling, adjusting cycle time as the bed ages instead of holding it fixed for the bed's whole life, is not a new idea. It has been described in the trade literature for years, for example in Hydrocarbon Processing. Extending adsorption cycles when bed condition allows can reduce regeneration frequency, extend adsorbent life and lower annual fuel use. A learned model makes the practice closed loop, proposing the next cycle from the current bed state rather than waiting for an offline schedule update. When switching follows bed condition, conservative margin can shrink without giving up protection.
Dehydration as a train-level constraint
A weakened bed forces a trade-off between feed rate and breakthrough risk. When adsorption capacity degrades, operators either cut feed to stay within margin or accept a higher risk of water reaching cryogenic service. That makes dehydration a constraint on the whole LNG train, and the cost grows when conservative operation becomes the default across shifts.
Bed-switching decisions interact with upstream solvent performance, contamination risk, downstream liquefaction demand and the aging profile of each vessel. Dehydration performance also sets the moisture that reaches a mercury removal unit placed downstream. A shared model gives operations, maintenance and engineering one view of those trade-offs instead of separate judgments. That plantwide view is hard to assemble from individual loop tuning, which is one reason fixed-schedule regeneration has lasted this long.
Building trust through advisory use
No model substitutes for the pattern recognition that comes from decades at the board. The number of variables shaping dehydration performance still exceeds what any operator can balance continuously by hand across multiple beds, changing feed conditions and train-level constraints.
In advisory mode the model recommends cycle changes and regeneration parameters, and operators decide whether each recommendation fits current plant conditions. Experienced operators can check the recommendation against what they see in moisture trends, pressure drop and upstream treating behavior. That kind of collaboration between people and AI can improve cross-shift consistency and give teams a common way to weigh trade-offs before the next move. Newer operators gain a consistent reference for decisions that used to depend on knowledge passed across shifts, which matters more as experienced board operators retire.
Advisory mode is a step toward closed loop. Trust builds through repeated exposure. When recommendations prove reliable across changing feed conditions and aging beds, the relationship moves from skepticism to verification. Closing the loop is then easier, because the control room has already seen how the model behaves under real operating pressure. In closed loop the model writes cycle and regeneration targets within limits the operators set, and they keep override authority.
How Imubit applies this
In gas processing and LNG, Imubit applies Map, Model and Control to the pretreatment section ahead of liquefaction. Map traces regeneration fuel, adsorbent life and throughput limits to the recurring decisions behind them, such as cycle timing and heating profiles. Model uses Deep Learning Process Control® (DLPC®) to learn bed behavior and its links to treating and liquefaction from the plant's own history, guided by first principles. Control takes those decisions to closed loop, writing setpoints to the existing APC or DCS, inside limits set by plant engineers.