Downstream of the mercury removal unit (MRU) in an LNG plant sits aluminum cryogenic equipment that is difficult and expensive to repair or replace. Mercury specifications in LNG service are stringent, yet MRUs in the field often fall short of expected performance under real operating conditions. Feed variability, moisture excursions and liquid carryover shift faster than conventional monitoring captures, and the gap between design basis and field performance keeps widening. Mercury removal performance depends on the whole conditioning train as much as on the guard bed.
How mercury damages cryogenic equipment
Mercury in feed gas is a direct plant reliability risk. It attacks aluminum cryogenic equipment through two overlapping mechanisms:
- Amalgamation. Mercury forms an amalgam with aluminum that disrupts its protective oxide layer. Once that layer is gone, the metal is open to rapid attack.
- Liquid metal embrittlement (LME). Mercury penetrates the aluminum oxide film and causes brittle fracture under tensile stress.
Both mechanisms act at the same time, and neither needs a large mercury concentration to start.
Brazed joints and welds concentrate the risk. Mercury collects at low points because of gravity and flow patterns, and residual fabrication stresses at welds supply the tensile component that LME requires. Neither mechanism shows itself until damage is well advanced, so specification limits sit far below the concentrations that would cause rapid failure.
Most LNG facilities set an internal mercury specification at or near 0.01 µg/Nm³. The limit exists to protect cryogenic equipment integrity and on-stream factor. The consequences of getting it wrong are well documented. Trace mercury accumulating in a cryogenic section caused a catastrophic heat exchanger failure at an LNG plant in Algeria in the 1970s, described by Digital Refining, and the incident shaped mercury specifications across the industry. The production lost in an unplanned shutdown is worth many times the cost of the MRU media.
Selecting an adsorbent for real LNG conditions
Adsorbent selection starts with the gas that actually reaches the bed. Mercury behavior in the field changes with speciation, moisture and contaminant carryover, and MRU beds run at the moderate temperatures and elevated pressures typical of gas processing service. A bed that looks adequate on paper loses life quickly when upstream liquid removal is inconsistent. Design basis and operating reality separate fast when feed composition shifts or upstream separation drifts.
Start with the feed
Adsorbents respond differently to elemental, oxidized and organic mercury, so a facility needs enough speciation data to know which forms are present. Where that data is incomplete, broader monitoring and a conservative selection basis work better than assuming one form dominates.
Feed source matters as much. Mercury content and speciation change as supply sources change, so regional averages are a weak basis for design at plants that receive gas from several sources or a changing supply mix. Site-specific measurement and ongoing monitoring give a stronger basis for sizing and for projecting sorbent life.
The main adsorbent families
- Sulfur-impregnated activated carbon is the most widely deployed option in LNG service because it is common and relatively low cost. Its weakness is moisture. Liquid water or condensate reduces capture and accelerates fouling, which makes upstream conditioning a direct factor in bed life.
- Copper sulfide on alumina tolerates wet service better and handles moisture excursions that would impair activated carbon.
- Silver-impregnated molecular sieve is regenerable. It carries a higher capital cost but different lifecycle economics, especially where regeneration offsets the recurring cost of replacement and disposal.
The differences show most when gas conditions are unstable, because tolerance to moisture and contaminants matters as much as nominal mercury capacity.
How upstream conditions limit adsorbent performance
Theoretical capacity counts for little if the adsorbent does not stay clean. Reported MRU cases describe pressure drop rising well above expected levels in service, together with heavy hydrocarbon condensation, sulfur leaching and fouling on the outlet side. Upstream coalescers and particulate filters often decide bed life as much as adsorbent chemistry does. A strong adsorbent choice still underperforms if liquids, solids or heavy hydrocarbons reach the bed often enough to blind active sites or restrict flow.
In brownfield plants where a standalone MRU is not practical, a silver-containing molecular sieve layer inside the existing dehydration vessels combines mercury protection and dehydration in one unit operation. That changes both the selection and the monitoring, because dehydration regeneration cycles then directly affect mercury capture.
Guard bed monitoring
Two adsorbent beds in a lead-lag configuration give continuous mercury protection and keep the train running during media changeouts. The lead bed does the primary capture and the lag bed is the backup. When the lead bed approaches saturation, it comes offline for media replacement, the former lag bed takes the lead, and the refreshed bed returns in the lag position.
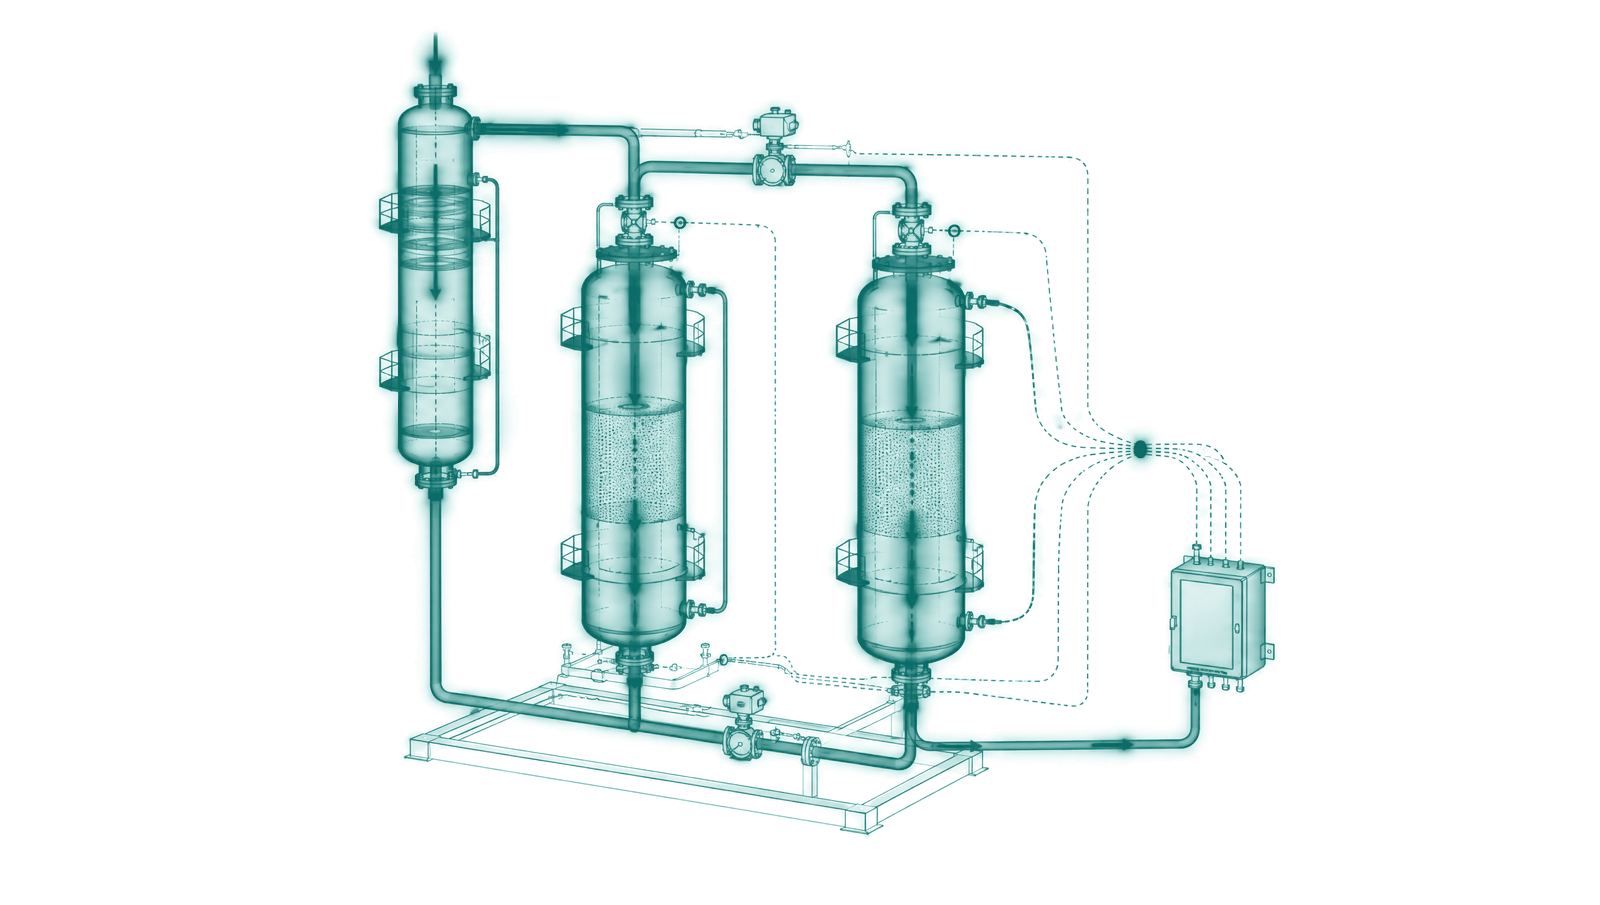
That arrangement protects the train during maintenance, provided bed condition is visible early enough to avoid running close to breakthrough.
Pair outlet concentration with differential pressure
The most useful monitoring pairs mercury concentration at the MRU outlet with differential pressure across the bed. Concentration confirms the bed still meets specification. Pressure trends reveal fouling or channeling that concentration misses. Together they give a more realistic picture of remaining bed life than either signal does on its own.
Read alongside upstream process data, the picture gets clearer still. A pressure rise that coincides with a coalescer upset means something different from one that builds gradually over months.
Read the rate of change
The trend rate tells as much as the absolute reading. A bed showing a steady, gradual pressure increase over six months is aging predictably. A sharp rise over two weeks points to an upstream upset that deposited liquids or particulates on the adsorbent. Telling these patterns apart decides whether the response is a scheduled changeout or an investigation of upstream separation performance.
Sampling frequency plays a direct part in that distinction. Continuous online mercury analyzers catch excursions that periodic grab samples miss entirely. The monitoring approach often decides whether an excursion is caught early or found after the bed is already compromised.
How train position shapes contamination risk
MRU placement relative to acid gas removal and molecular sieve dehydration varies by process design, and it determines which contamination risks monitoring has to catch. An MRU placed earlier in the train is exposed to CO₂, H₂S or free water, any of which impairs the adsorbent through competitive adsorption or fouling.
The equipment ahead of the MRU acts as bed protection. High-efficiency coalescers and fine particulate filters limit liquid and solids carryover, and dehydration performance controls the moisture reaching the bed.
Dehydration upsets show up quickly at the MRU. Regeneration timing problems or sieve carryover during switchover send moisture downstream before anyone sees it in the dehydration data. Tracking the dehydration operating strategy upstream gives an early signal that MRU performance may shift. Monitoring each piece of equipment on its own does not give that cross-unit view.
Coordinating operations, maintenance and procurement
Guard bed monitoring is worth more when operations, maintenance and procurement work from the same condition data:
- Operations tracks breakthrough and differential pressure to identify beds approaching end of life.
- Maintenance uses the same indicators to align changeouts with planned windows instead of conservative calendar intervals.
- Procurement orders sorbent against expected replacement dates rather than carrying excess inventory.
When each team works from its own assumptions about what is driving pressure drop or breakthrough, changeout timing drifts toward one of two outcomes. Premature replacement wastes sorbent. Delayed response risks a specification exceedance. Shared condition data avoids both, because the trends that tell operations a bed is aging also tell maintenance when to schedule the work and procurement when to order the media.
Alignment also lowers the risk of a bed reaching end of life just before a planned turnaround, when resources and attention are already stretched. It brings MRU changeouts into the same planning cycle as the rest of the conditioning train's maintenance, rather than treating them as standalone events. Knowledge management practices that keep speciation data and changeout history together inform both the initial adsorbent selection and replacement timing over the bed's service life.
Cross-unit visibility from a learned model
A model learned from the plant's own data across the inlet separators, dehydration and mercury removal can find relationships between changing feed conditions and MRU performance that conventional monitoring misses. In advisory mode it recommends targets for upstream conditioning variables, such as coalescer differential pressure limits, dehydration regeneration timing and inlet separator levels. Operators review each recommendation before acting on it.
The model does not stand in for the judgment that comes from years of running a specific facility's conditioning train. It puts the cross-unit trade-offs in one view, so operations, maintenance and planning work from the same picture instead of interpreting separate data streams. Collaboration between people and AI built on that shared view fits environments where trust is earned through evidence over time.
How Imubit applies this
Imubit applies Map, Model and Control to feed gas conditioning in gas processing and LNG. Map traces guard bed life, changeout cost and throughput risk to the recurring decisions behind them, such as coalescer limits and dehydration regeneration timing. Model uses Deep Learning Process Control® (DLPC®) to learn the conditioning train's behavior from its own history, guided by first principles. Control takes those decisions from advisory recommendations to closed loop, writing setpoints to the existing APC or DCS, inside limits set by plant engineers.