Process plants run heat-intensive equipment around the clock, and every operating decision carries a carbon cost. A fired heater adjusted conservatively, compressors cycling, or a steam system running away from its best conditions burns more fuel than necessary, shift after shift. Operations leaders are asked to cut emissions without giving up throughput or margin, and they are often asked whether industrial AI is itself part of the problem.
The concern is reasonable. The IEA projects that data center electricity demand will more than double by 2030. The IEA also estimates that widespread adoption of existing AI applications in end-use sectors, industry among them, could cut CO₂ emissions by 1,400 million tonnes in 2035.
For a plant evaluating AI, the practical question is whether the emissions it avoids in operations outweigh the carbon cost of the technology. The evidence says yes, provided AI is applied where the reductions are largest.
The carbon footprint of AI, in context
The cost of AI infrastructure deserves honest accounting. The IEA puts current indirect emissions from data centers at around 180 million tonnes of CO₂ a year, rising to about 300 million tonnes by 2035 in its base case.
In proportion, the IEA estimates data center emissions at about 0.5% of global fuel combustion CO₂ today, and below 1.5% through 2035 even in its rapid-growth scenarios. On the IEA's figures, the potential reductions from AI in end-use sectors are three to four times the total emissions of data centers, depending on how fast data center demand grows.
The difference is clearer at plant level. A single process plant may run dozens of fired heaters and boilers continuously, together firing tens to hundreds of megawatts of heat. The computing needed to run an optimization model for that plant draws a small fraction of that energy. When the model reduces fuel consumption by even a few percent, the avoided emissions exceed the model's electricity footprint by orders of magnitude. For energy-intensive operations, the comparison is not close.
Where industrial AI reduces the most carbon
Process plants generate Scope 1 emissions continuously, from furnaces burning fuel, compressors cycling and steam systems running around the clock. A model learned from the plant's own operating data, guided by first principles, can capture the relationships between hundreds of interacting variables: feed composition, ambient conditions, equipment states and energy use. Those relationships are too complex and change too quickly for operators to optimize by hand, especially across several units at once, and a generic model built on design assumptions misses many of them.
The largest reductions come from three areas.
Energy in heat-intensive equipment
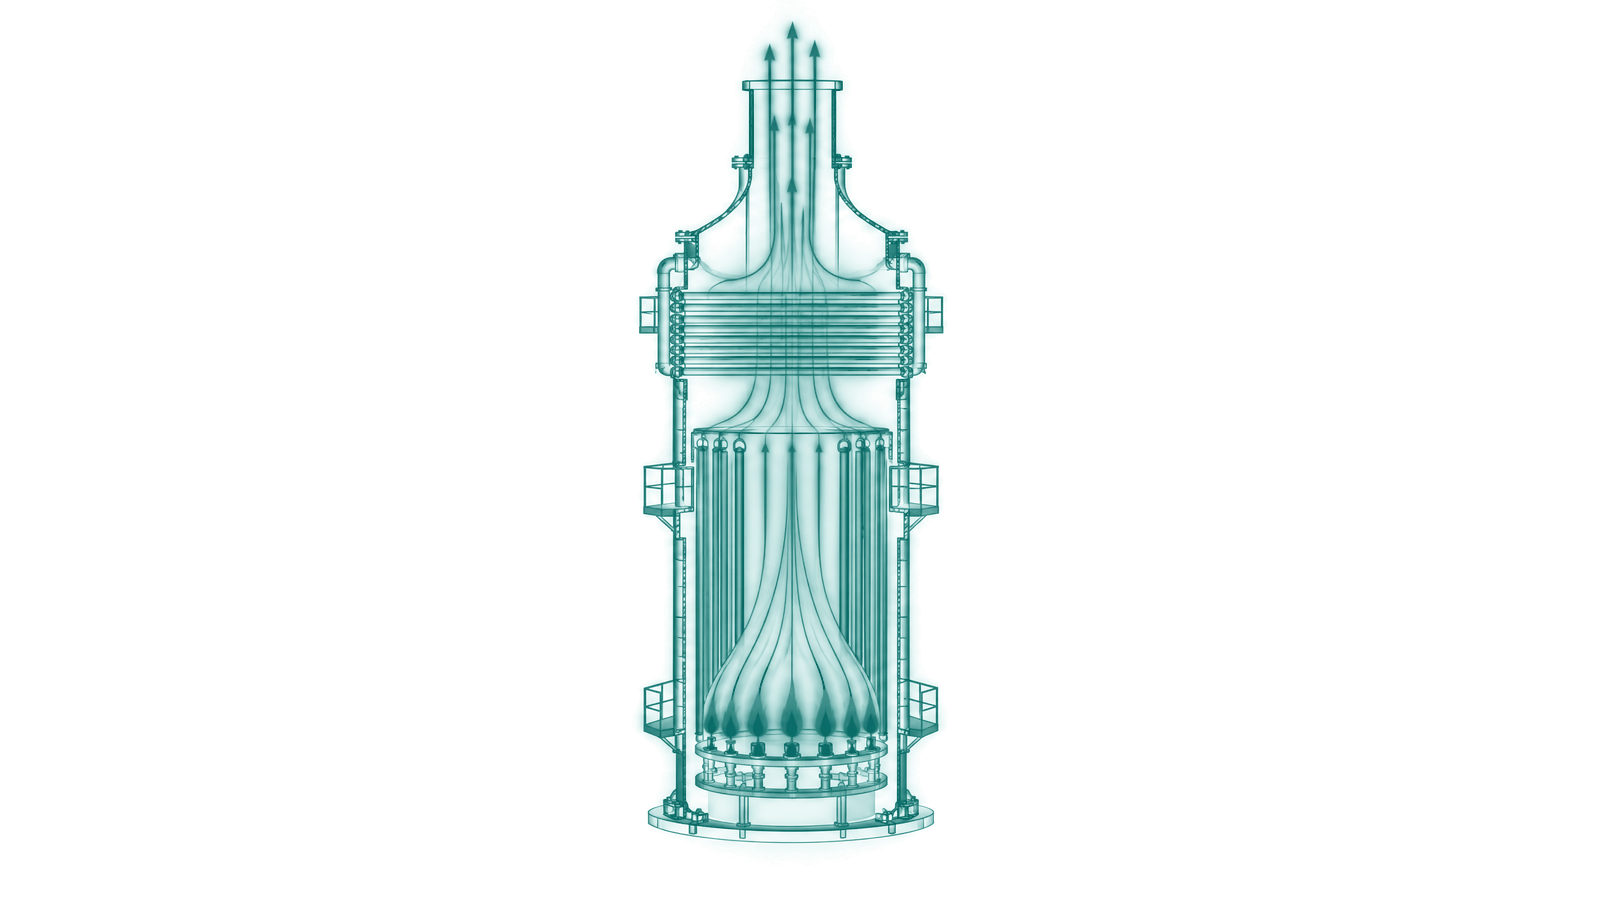
A learned controller can adjust setpoints on furnaces, kilns, boilers and compressors continuously as conditions change, which lowers fuel consumption per unit of output. Because it responds to current feed quality, ambient temperature and equipment condition, it tracks how the plant runs today, where a static model degrades as conditions move away from its design point.
Feedstock conversion and yield
A modest improvement in conversion means more saleable product from the same feed. Less reprocessing, fewer off-spec runs and lower energy per tonne all reduce emissions without capital upgrades. A unit that converts feed more efficiently lowers its energy-to-output ratio, so production efficiency and carbon intensity improve together.
When fewer tonnes need reprocessing, the plant avoids both the energy of the original run and the extra energy of the rework. For plants that run several product grades, a model can also identify the campaign sequences that use the least total energy across transitions.
Carbon and yield goals are more complementary than they often appear. A model that optimizes for overall economics tends to favor lower energy use and higher yield, because both raise margin per tonne.
Process stability and run length
Each unplanned shutdown creates a surge of emissions from venting, flaring and full-fire restart sequences. Depending on the unit, the carbon cost of a single emergency trip can equal days or weeks of normal operating emissions. A model that picks up early signs of fouling or equipment drift helps keep units inside safe operating limits for longer, so fewer of those spikes occur. The same approach supports plant reliability more broadly.
A unit that runs more stably also converts feed more efficiently and uses less energy per tonne of output. Plants with wide variability between shifts, or units with older control schemes, usually have the most room to improve.
Making emissions visible before they become costs
Visibility is one of the less discussed constraints in industrial decarbonization. Many plants track total energy spend but have no real-time view of emission intensity per unit, per product or per shift. Without that detail, teams cannot tell which operating changes would cut the most.
A model that brings together process data, utility consumption and lab results changes that. Operations can see which units emit the most CO₂ per tonne of throughput, and planning can evaluate how changes in product mix affect overall emission intensity.
Where the quick wins are
The largest reductions often sit at the boundaries between decisions made by different teams. A maintenance deferral that looks reasonable on its own can push a furnace to burn more fuel for weeks. A production target that maximizes throughput on one unit can raise energy intensity across the plant.
When those trade-offs are visible in one operational view, the quick wins show up: excess oxygen in fired heaters, undetected steam leaks, and operating modes that use a disproportionate share of energy. Each can be corrected without capital once the right information reaches the right team in time.
Why most AI emissions efforts stall before scale
The main constraint is adoption, and many organizations never take AI for emissions past the pilot.
Pilots that scale tend to share a few traits. They start on a specific unit where energy waste is visible and measurable, and widen from there. Operators see advisory recommendations before the model runs in closed loop, and trust builds as those recommendations prove accurate over time. When operators see the model recommending the moves they would have made, plus a few they had not considered, confidence grows.
They also connect emission reductions to the financial measures operations leaders already track: fuel cost per tonne, energy per unit and throughput per shift. In a process plant, carbon reduction is largely an operational efficiency program with environmental co-benefits. Every unit of energy not consumed is both a cost reduction and an emission reduction, so the business case does not rest on carbon pricing or regulation alone.
The IEA has noted that there is currently no momentum to ensure widespread adoption of these AI applications, and that their aggregate impact could stay marginal without the right enabling conditions. For an individual plant, those conditions are practical: plant data that is clean enough, operators willing to evaluate the recommendations, and a starting point where the value is obvious.
How the Imubit Platform applies
The Imubit Platform treats energy and emissions as part of the same operating decisions, in refining, chemicals and polymers, cement, and mining and minerals. Map traces where fuel and energy are lost to recurring decisions, Model learns each unit's causality from its own history with Deep Learning Process Control® (DLPC®), and Control writes setpoints through the existing APC and DCS in closed loop. Where energy is the optimization target, deployments have delivered a 15 to 30% reduction in energy consumption. See how the platform works.